Mon – Fri: 8:00am – 5:00pm

Archives for September 2026

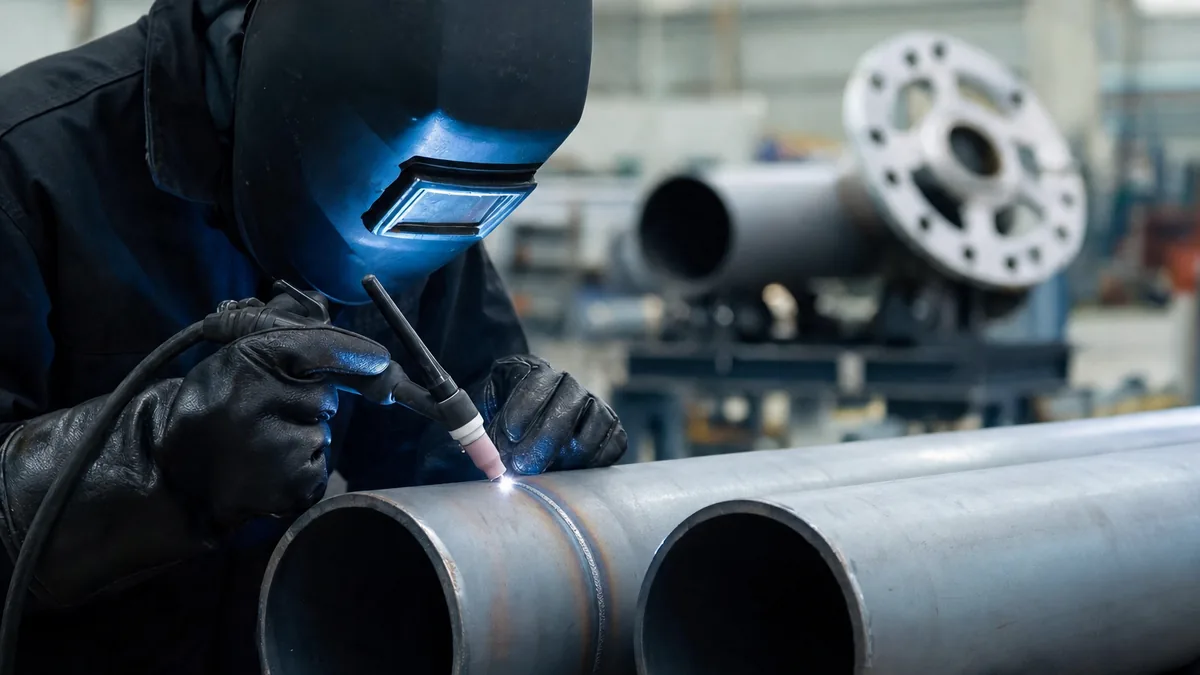
Welder TIG welding the butt joint of a carbon steel pipe spool on pipe stands in a fabrication shop

Pressure Welding in Alberta: How Piping, Vessels and Skids Fit Together

Overview

If you’re buying welding or fabrication work that involves pressure, the terms can get confusing fast. Pressure welding, B pressure, process piping, pressure vessels and skids all get mentioned in the same conversation, and they overlap. This guide explains what each one means, how they connect, and what to ask before you hire a shop. It’s written for plant managers, contractors and project owners in Calgary and across Alberta.
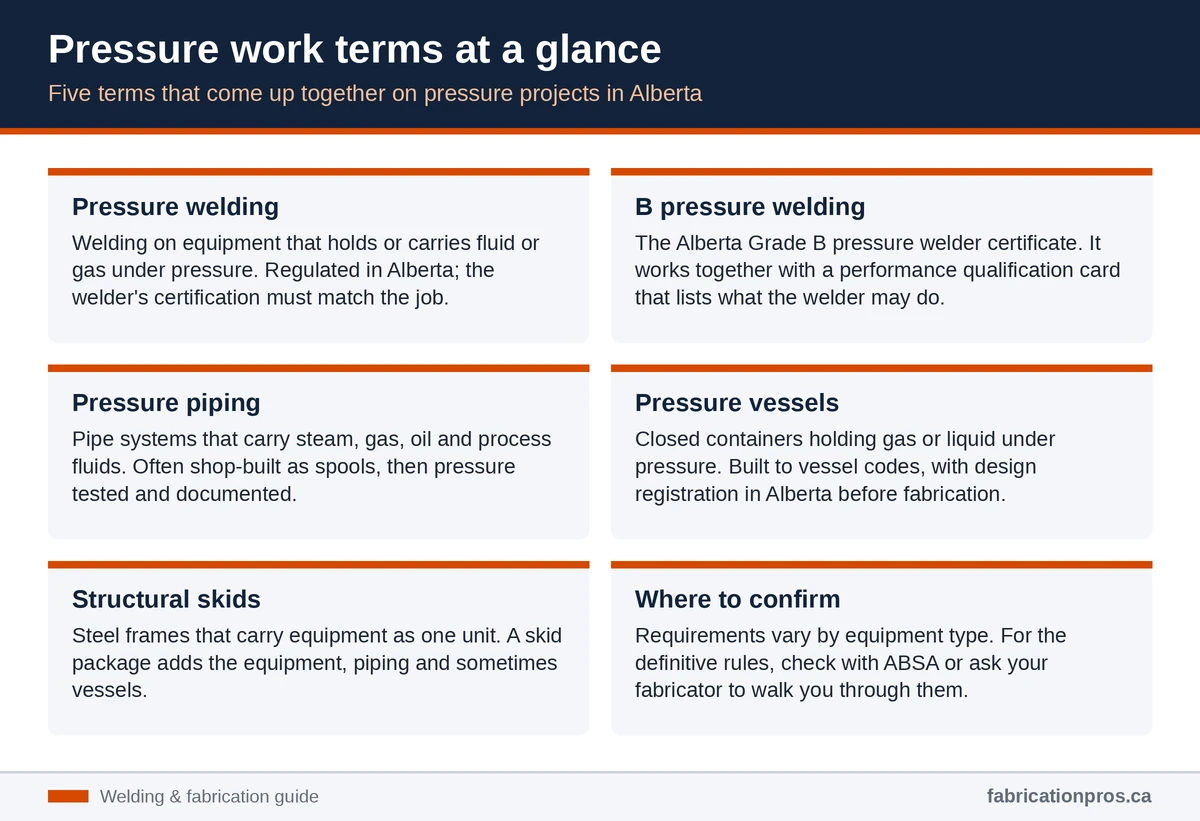
Infographic explaining pressure welding, B pressure welding, pressure piping, pressure vessels and structural skids
Five terms that usually come up together on Alberta pressure projects.

What is pressure welding?

In everyday shop talk, “pressure welding” means welding on equipment that holds or carries fluid or gas under pressure. That includes boilers, pressure vessels and pressure piping. A failed weld on a pressure system can release stored energy suddenly, so the work is held to a higher standard than ordinary structural welding.

In Alberta, this work is regulated under the provincial Safety Codes Act, and ABSA (the Alberta Boilers Safety Association) administers pressure equipment safety. Welders who work on pressure equipment need the right ABSA certification, and the qualification has to match the job. The exact rules depend on the type of equipment, so it’s always worth confirming the requirements for your specific project.

What is B pressure welding?

“B pressure” refers to the Grade B pressure welder certificate issued in Alberta. According to ABSA’s Grade B information, candidates are generally journeyman or Red Seal welders, or third-year welding apprentices applying through their school.

The certificate works together with a performance qualification card. The card lists what the welder is actually authorized to do, such as the welding process, materials and limits on the work. In other words, holding a B ticket isn’t a blanket approval. What matters is whether the welder’s card covers your specific weld. Learn more on our B pressure welding services page.

Pressure piping: moving fluids and gases safely

Pressure piping is the network of pipe that carries steam, gas, oil, chemicals and other process fluids. In shops it’s often built as pipe spools: sections fabricated in a controlled shop environment and then installed and connected on site. Fabricating spools in the shop generally makes it easier to control weld quality and testing.

ABSA notes that ASME B31.3, the process piping code, is adopted in Alberta for process piping where it applies. Piping construction in the province also typically involves registered welding procedures, pressure testing (commonly hydrostatic testing) and documentation of the finished work.

Different welding processes are used depending on the pipe and the job. If you’d like a plain-language overview, see our guides to TIG (GTAW) welding and stick (SMAW) welding. For the full service, visit our high-pressure process piping fabrication page. Stainless piping has its own requirements, covered on our stainless steel welding page.

Pressure vessel fabrication

A pressure vessel is a closed container that holds gas or liquid at a pressure different from the surrounding air. Air receivers, separators and heat exchanger shells are common examples. Because the contents are under pressure, vessels are built to recognized design codes, most commonly ASME Section VIII, Division 1 or CSA B51.

Alberta also requires pressure vessel designs to be registered, and ABSA’s guidance says the submitted drawings need to show the design conditions and loadings. That step happens before the vessel is built, which is why it pays to bring your fabricator in early. Our pressure vessel fabrication services page covers what we build.

Structural skids and skid packages

A skid is a steel frame that carries equipment so it can be built, moved and installed as one unit. Pump skids, compressor skids and generator skids are common. A skid package goes a step further, combining the frame with equipment, piping and sometimes vessels, so the customer receives a complete assembly.

This is where the topics in this guide meet. The steel frame is structural work. Any pressure piping or vessels mounted on the skid fall under the pressure equipment rules above. Building both together in one shop can simplify coordination. See our oil field skid packages page, and our structural beam, column and truss fabrication page for the structural side.
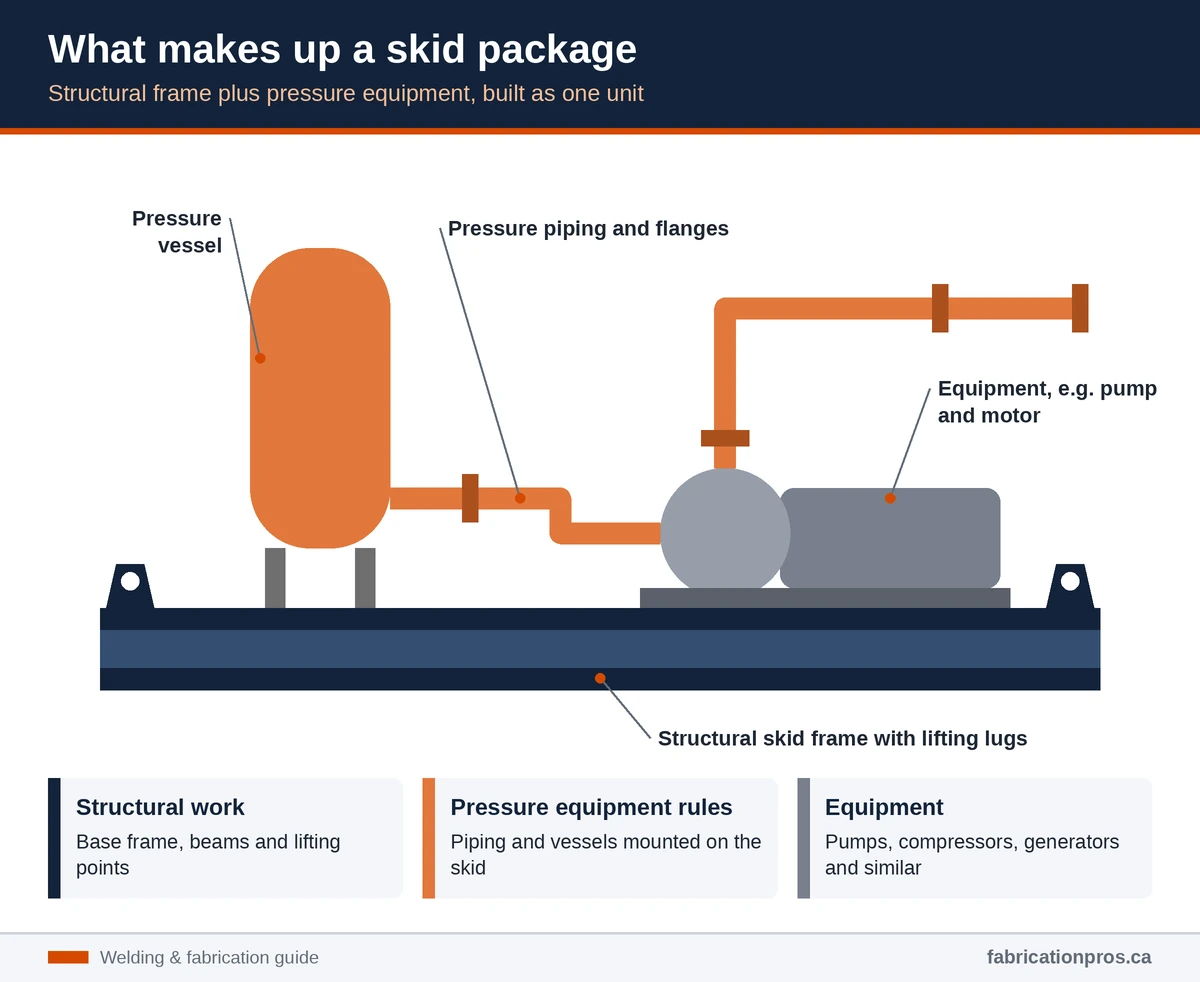
Diagram of a skid package showing the structural frame, pressure vessel, pressure piping and pump
The skid frame is structural work; the piping and vessel on it fall under pressure equipment rules.

How it all fits together

TopicWhat it isKey thing to know
Pressure weldingWelding on equipment that contains pressureRegulated in Alberta; welder certification must match the job
B pressure weldingGrade B pressure welder certificationWorks with a performance qualification card
Pressure pipingPipe systems carrying fluids and gasesBuilt to piping codes; tested and documented
Pressure vesselsClosed containers holding pressureBuilt to vessel codes; design registration in Alberta
Structural skidsSteel frames carrying equipmentOften combine structure, piping and vessels

Questions to ask before hiring a fabricator

Whoever you choose, these questions help you compare shops fairly:

  1. Do the welders’ certifications and qualification cards cover the process and material for my job?
  2. Which codes will the work be built to, and who handles registration and documentation?
  3. What inspection and testing will be done, and what paperwork will I receive at the end?
  4. Can the work be done in the shop, on site, or both?
  5. Who coordinates the structural, piping and vessel work if they’re all part of one package?

Requirements vary by project and equipment type, so treat this guide as an overview. For the definitive rules, check with ABSA or ask your fabricator to walk you through them.

Shop work and on-site work

Many pressure jobs mix both. Spools, vessels and skids are commonly built in the shop, while tie-ins, repairs and modifications happen at the facility. If you’re working on an oilfield site, see our rig welding services, and for repairs at your location, our mobile welding repair service.

Talk to us about your project

If you’re planning pressure piping, a vessel, a skid or repair work in Calgary or southern Alberta, we’re happy to talk it through. Visit the Fabrication Pros homepage to see all our services, or contact us for a free quote.

Contact us with any questions you may have.

No file chosen

Read more
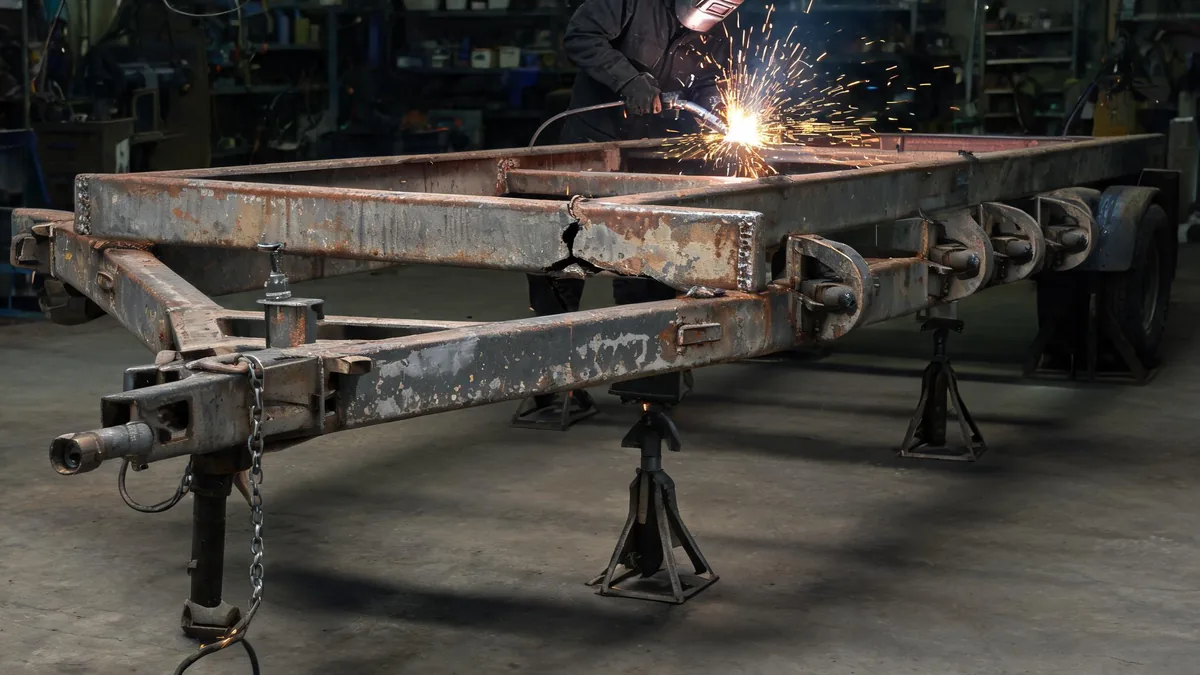
Welder MIG welding a cracked crossmember on a steel utility trailer frame raised on stands

Trailer Frame and Hitch Repair in Calgary: When Welding Is Needed

Overview

A trailer works hard and rarely gets a day off. It hauls heavy loads over rough roads, sits out in Alberta winters and takes knocks at every job site. Sooner or later something cracks, bends or wears out. Knowing which problems are minor and which are safety issues helps you decide when to call a welder.

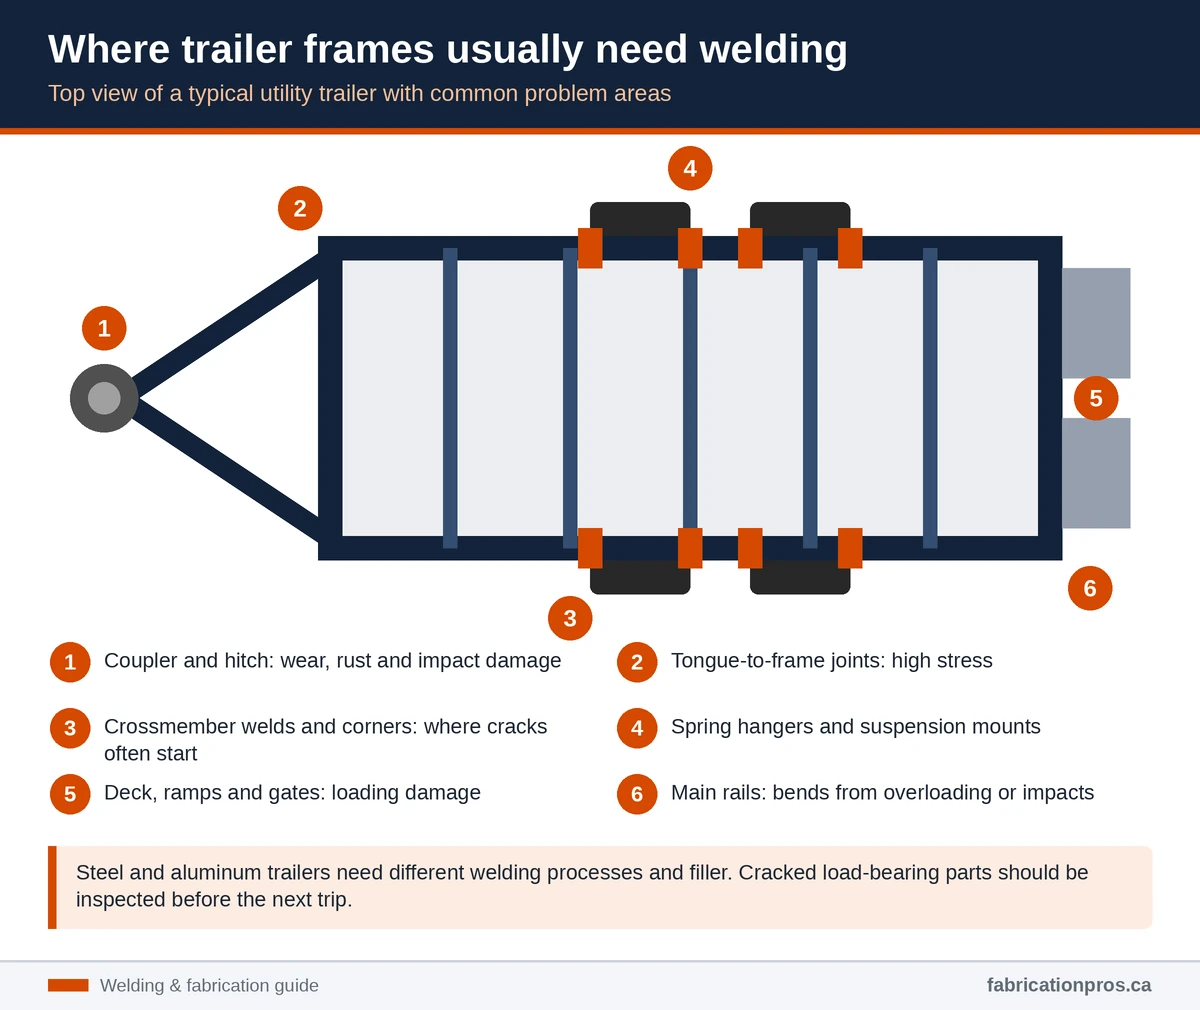
Common trailer problems that call for welding

  • Cracked frame welds or frame members. Cracks often start at existing welds or at stress points such as corners and crossmembers.
  • Bent or damaged frames. Overloading, impacts and jackknifing can twist or bend the frame.
  • Damaged hitches and couplers. Wear, rust and impact damage can weaken the parts that connect the trailer to the truck.
  • Broken suspension mounts and spring hangers. These take constant load and vibration.
  • Damaged decks, ramps and gates. Loading equipment onto a trailer is hard on steel and aluminum decking.
  • Cracks in aluminum trailers. Aluminum can crack from fatigue and needs the right welding process and filler.
Top-view diagram of a utility trailer frame marking the coupler, tongue joints, crossmembers, spring hangers, ramps and main rails
Common problem areas on a utility trailer frame, from the coupler back to the ramps.

Warning signs to watch for

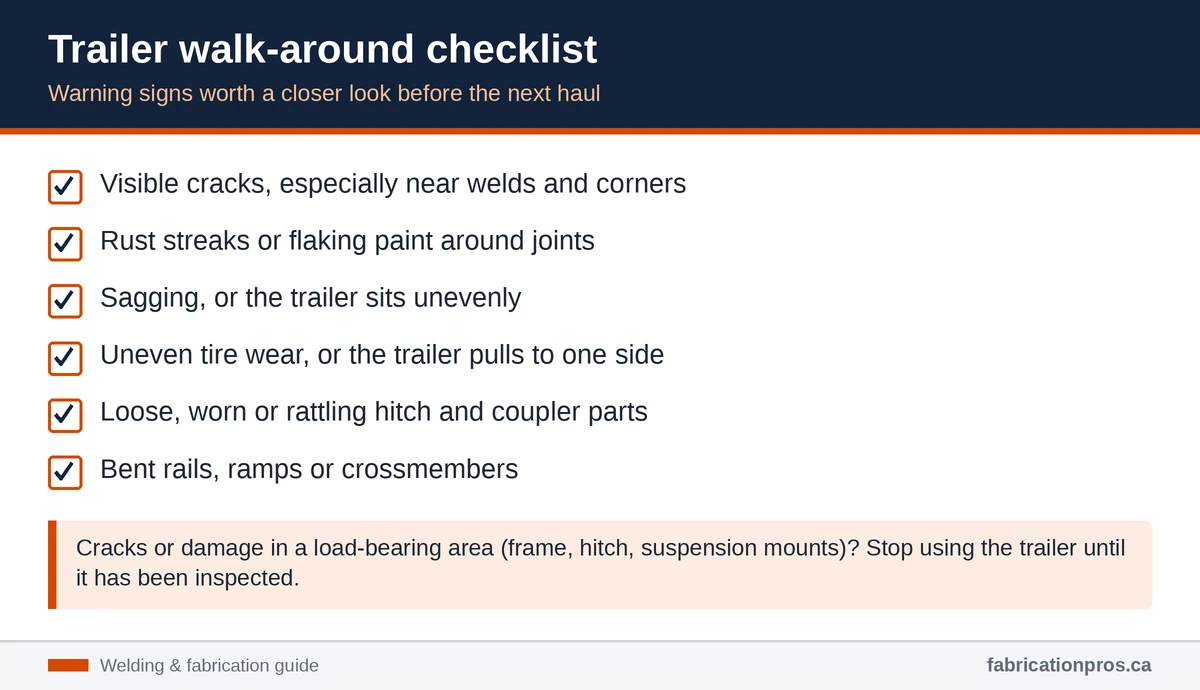
Catching a problem early is almost always cheaper and safer. During a walk-around, look for:

  • Visible cracks, especially near welds and corners
  • Rust streaks or flaking around joints
  • Sagging or uneven sitting height
  • Uneven tire wear or a trailer that pulls to one side
  • Loose, worn or rattling hitch and coupler parts
  • Bent rails, ramps or crossmembers
Checklist of trailer warning signs: cracks near welds, rust streaks, sagging, uneven tire wear, loose hitch parts and bent rails
A quick walk-around before each haul catches most problems early.

Why trailer repairs are a safety matter

Trailer frames, hitches and suspension parts carry the load and keep the trailer attached to the truck. A weak weld in one of these areas can fail under stress, and that can be dangerous on the highway. If you notice cracks or damage in a load-bearing area, it’s best to stop using the trailer until it’s been inspected.

Steel or aluminum: does it matter?

Yes. Steel and aluminum trailers behave differently and call for different welding techniques and filler materials. Aluminum in particular needs careful preparation and the right process. If you’d like to understand why, read our guide on why aluminum welding is different from steel, or see our aluminum welding services.

Repair on site or in the shop?

Many trailer repairs can be done where the trailer sits, which saves you hauling a damaged trailer anywhere. Our mobile welding repair and portable welding services travel to sites in and around Calgary. Larger structural repairs and modifications may be better done in the shop, where the trailer can be supported properly. A welder can tell you which makes sense once they’ve seen it.

Repairs, upgrades and custom work

Repair isn’t the only option. Trailers can also be modified, for example with added reinforcement, tie-down points, ramps or racks, to suit the work you do. If your trailer hauls equipment, see our heavy equipment welding and repair work, and our rig welding services for oilfield sites.

Get your trailer looked at

If your trailer has a crack, a bend or a worn hitch, we can take a look. See our full trailer welding repair services, visit the Fabrication Pros homepage, or contact us for a free quote.

Still deciding what kind of help you need? Our planning guide to welding and fabrication services in Calgary compares shop work, on-site work and fabrication.

Contact us with any questions you may have.

No file chosen

Read more
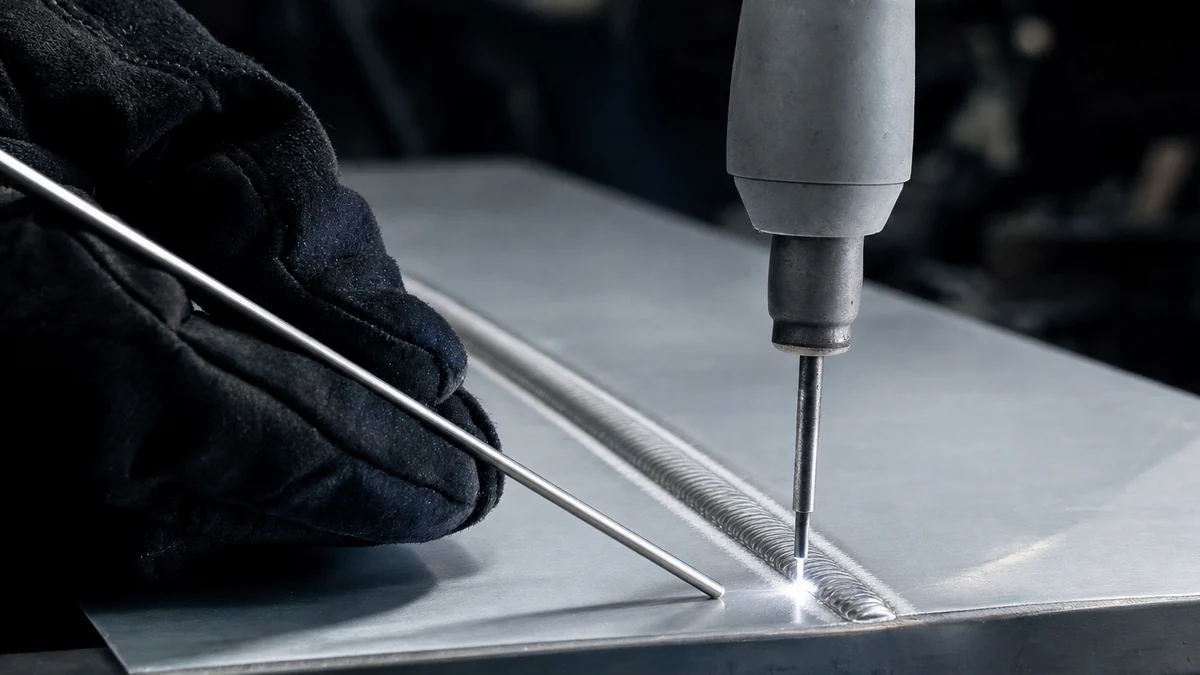
Close-up of TIG welding aluminum plate with a filler rod fed into the weld pool

Why Aluminum Welding Is Different From Steel

Overview

Aluminum and steel might look like they’d weld in much the same way. They don’t. Aluminum is lighter and resists rust, which is why it’s so common on trailers, fuel tanks, boats and food equipment, but it behaves very differently under a welding arc. Knowing why helps you understand what a good aluminum weld requires and why not every welder or shop does it well.

The oxide layer

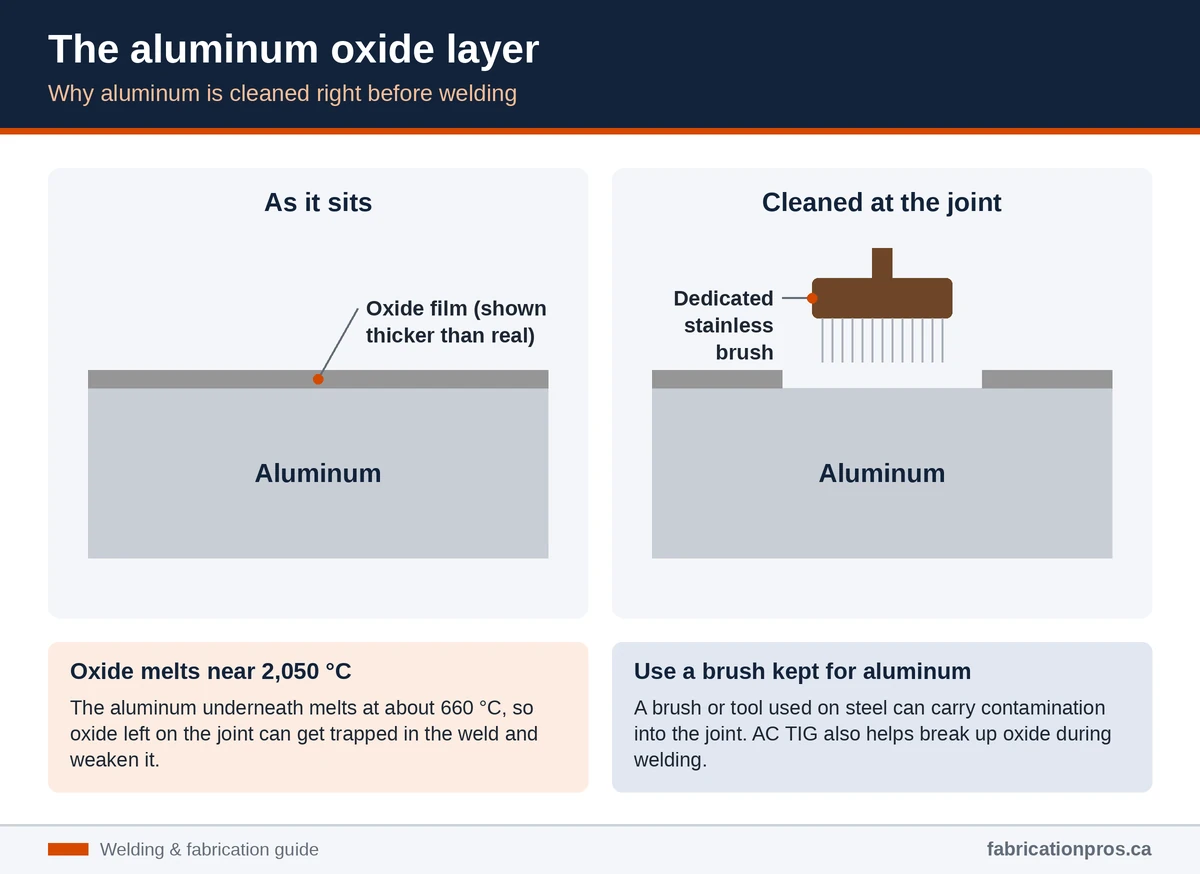
Aluminum forms a thin, tough oxide layer on its surface almost immediately. That layer melts at a much higher temperature than the aluminum underneath it. If the oxide isn’t removed before welding, it can get trapped in the weld and weaken it. That’s why aluminum has to be cleaned carefully before welding, using a dedicated stainless steel brush or other suitable cleaning method rather than a tool that’s been used on other metals.

Diagram of the oxide film on aluminum, which melts near 2,050 °C while aluminum melts at about 660 °C, and cleaning with a dedicated stainless brush
The oxide skin melts at a far higher temperature than the aluminum under it.

Heat behaves differently

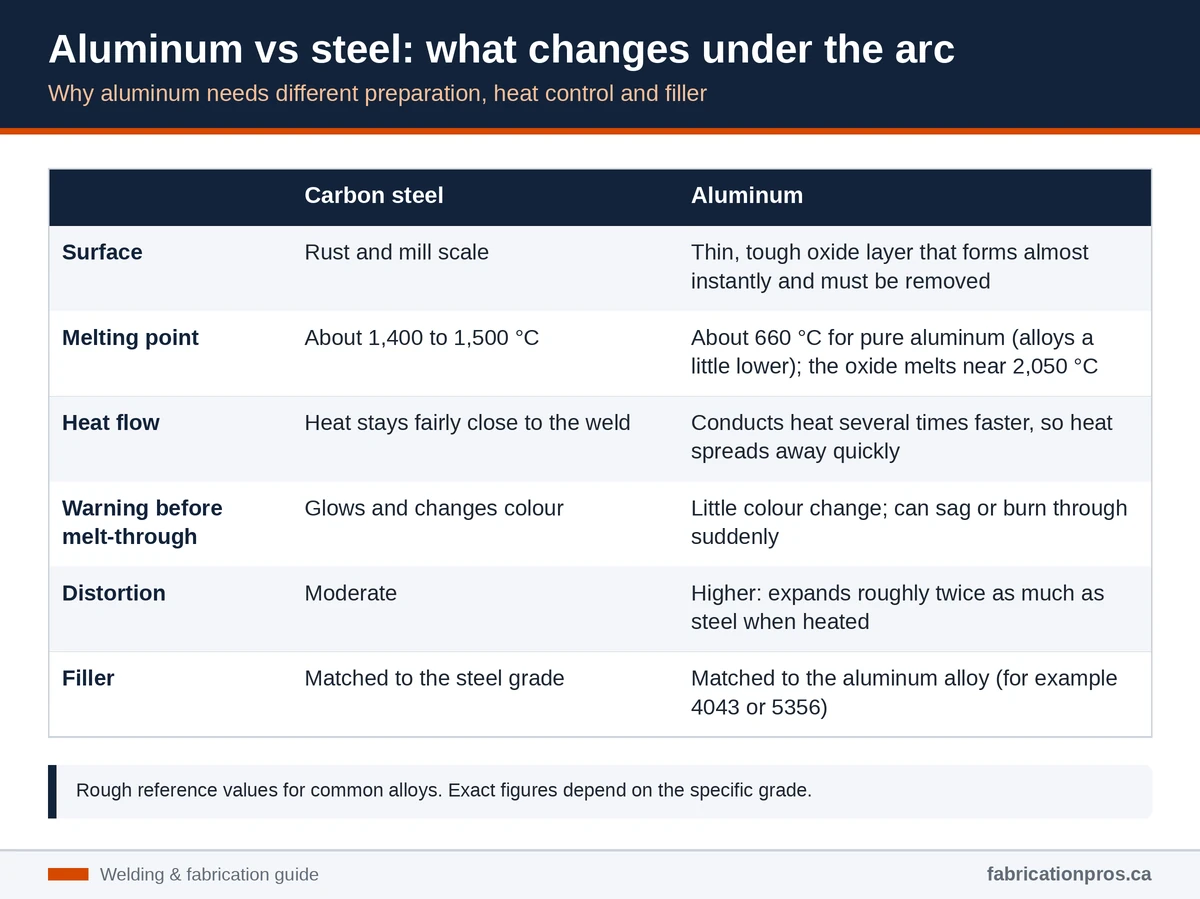
Aluminum conducts heat far better than steel. Heat spreads quickly away from the weld, so more heat input is often needed to get started. But aluminum also melts at a lower temperature than steel and gives little warning before it sags or burns through. Controlling heat is a big part of the skill, especially on thin material.

It’s softer and moves more

Aluminum expands more when heated than steel does, so parts can distort as they heat and cool. Careful fit-up, clamping and welding sequence help keep the finished piece straight. Because aluminum is softer, it’s also easier to damage while handling and preparing.

Comparison chart of carbon steel and aluminum: surface oxide, melting point, heat flow, melt-through warning, distortion and filler
How aluminum differs from steel once the arc is on.

Filler metal matters

Different aluminum alloys need different filler metals, and the wrong choice can cause cracking or a weaker joint. We cover this in more detail in our post on the difference between aluminum filler alloys.

Welding processes for aluminum

Aluminum is commonly welded with TIG (GTAW) or MIG (GMAW), and each has its place. TIG gives fine control and is often chosen for thin material and visible, precise welds. MIG is faster and suits longer runs and thicker material. Learn more in our guide to TIG (GTAW) welding.

SteelAluminum
SurfaceRust and scaleTough oxide layer that must be removed
HeatStays near the weldSpreads quickly, burns through easily
DistortionModerateHigher; needs careful control
FillerMatched to steel gradeMatched to the aluminum alloy

Where aluminum welding is used

Stainless steel has its own set of challenges, which we cover on our stainless steel welding page.

What to ask before you hire someone

  1. Does the shop regularly weld aluminum, or mostly steel?
  2. Which process will be used, and why?
  3. Will the aluminum be cleaned and prepared properly?
  4. Can they repair it on site, or does it need to come to the shop?

Talk to us about your aluminum project

Whether it’s a cracked part, a custom build or a repair, we can help. See our aluminum welding services in Calgary, our mobile welding repair, the Fabrication Pros homepage, or contact us for a free quote.

Contact us with any questions you may have.

No file chosen

Read more
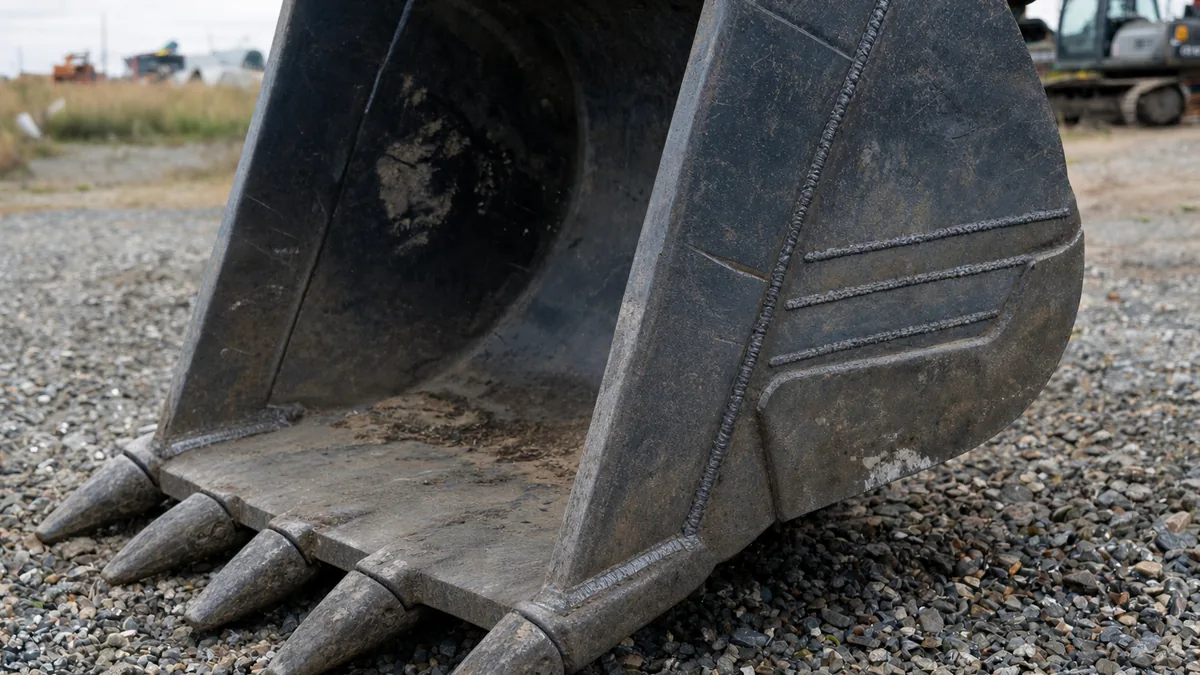
Excavator bucket cutting edge, corners and side cutters covered in hard facing weld beads

What Is Hard Facing on Excavators and Loader Buckets?

Overview

If you run an excavator or loader in Calgary, you already know what gravel, clay and rock do to steel. Cutting edges round over, corners thin out and buckets wear faster than anyone would like. Hard facing is one of the most effective ways to slow that wear down, and it’s a service we perform every day at Fabrication Pros.

What is hard facing?

Hard facing (also written “hard facing”) means welding a wear-resistant layer onto the surface of a part that takes a beating. The layer is harder than the steel underneath it, so instead of the bucket wearing away, the hard-faced surface takes the abuse. The base metal keeps its strength and the part lasts longer.

Where hard facing is used on a bucket

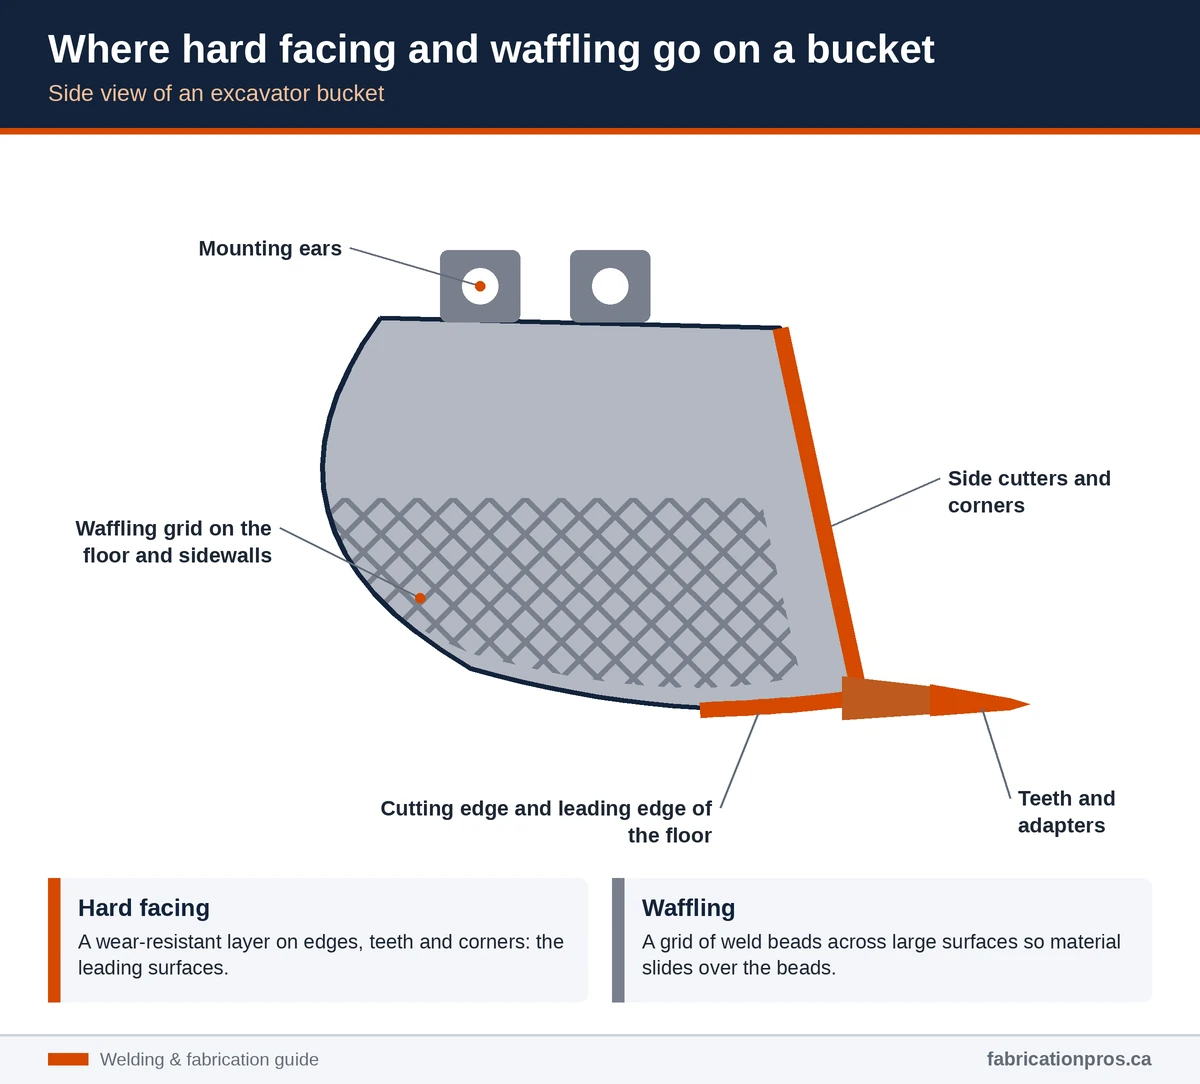
Hard facing goes where wear is worst. On excavator and loader buckets that usually means:

  • Cutting edges
  • Side cutters and corners
  • Teeth and adapters
  • The leading edge of the bucket floor
  • Other areas that constantly grind against material
Side-view diagram of an excavator bucket showing hard facing on the cutting edge, teeth, side cutters and corners, and waffling on the floor and sidewalls
Hard facing protects the leading edges; waffling protects the large flat surfaces.

What kind of wear does hard facing fight?

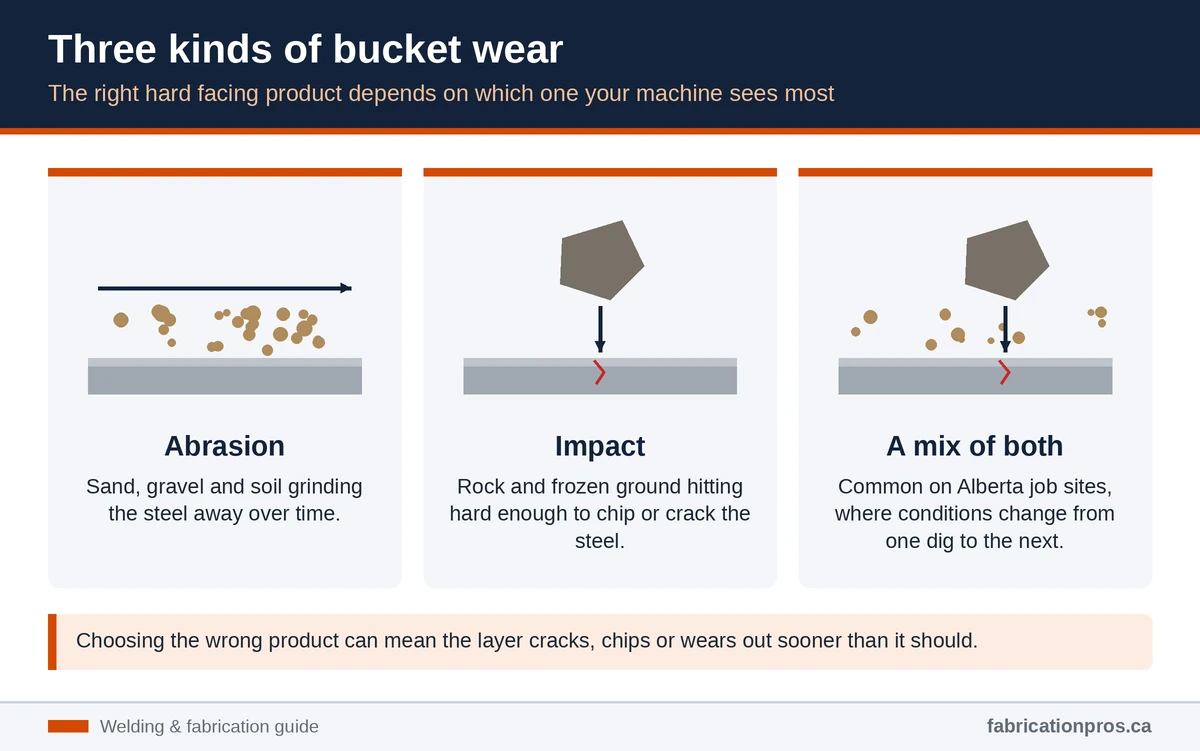
Different digging conditions damage steel in different ways:

  • Abrasion: sand, gravel and soil grinding the steel away over time.
  • Impact: rock and frozen ground hitting the bucket hard enough to chip or crack it.
  • A mix of both: common on Alberta job sites, where conditions change from one dig to the next.

The right hard facing product depends on which of these your machine faces most. Choosing the wrong one can mean the layer cracks, chips or wears out sooner than it should, which is why the material and technique matter as much as the weld itself.

Infographic of the three kinds of bucket wear: abrasion, impact, and a mix of both
The type of wear decides which hard facing product makes sense.

Hard facing vs. waffling

People often ask how hard facing differs from waffling. They work together rather than compete. Hard facing puts a wear-resistant layer on edges, teeth and corners. Waffling lays a grid of weld beads across the bucket’s floor and sides so material slides over the beads instead of grinding directly on the steel. Many buckets benefit from both.

Hard facingWaffling
What it isWear-resistant weld layerGrid pattern of weld beads
Typical locationEdges, teeth, cornersFloor and sidewalls
Main purposeResist abrasion on leading surfacesProtect large surfaces from sliding wear

When should a bucket be hard faced?

The best time is before the wear becomes serious. Hard facing a new or rebuilt bucket helps protect the steel from day one. On a used bucket, it works best while the base metal is still in good shape. If the bucket is badly worn through, cracked or warped, it may need repair first, or replacement. Not sure which applies to yours? Have it looked at before the damage gets worse.

Hard facing in the shop or on your job site

Downtime costs money, so we come to you when that makes sense. Our mobile welding repair service covers Calgary and surrounding areas, and larger jobs can be handled in the shop. If you want a broader look at what we do for excavators, loaders, dozers and attachments, see our heavy equipment welding and repair page.

Get your bucket looked at

If your bucket edges are rounding over or you want to protect a new one, we can help. Visit the Fabrication Pros homepage to see all our welding and fabrication services, or contact us for a free quote.

Not sure whether a worn bucket is still worth saving? Our article on when to repair or replace an excavator or loader bucket walks through the signs to look for.

Contact us with any questions you may have.

No file chosen

Read more
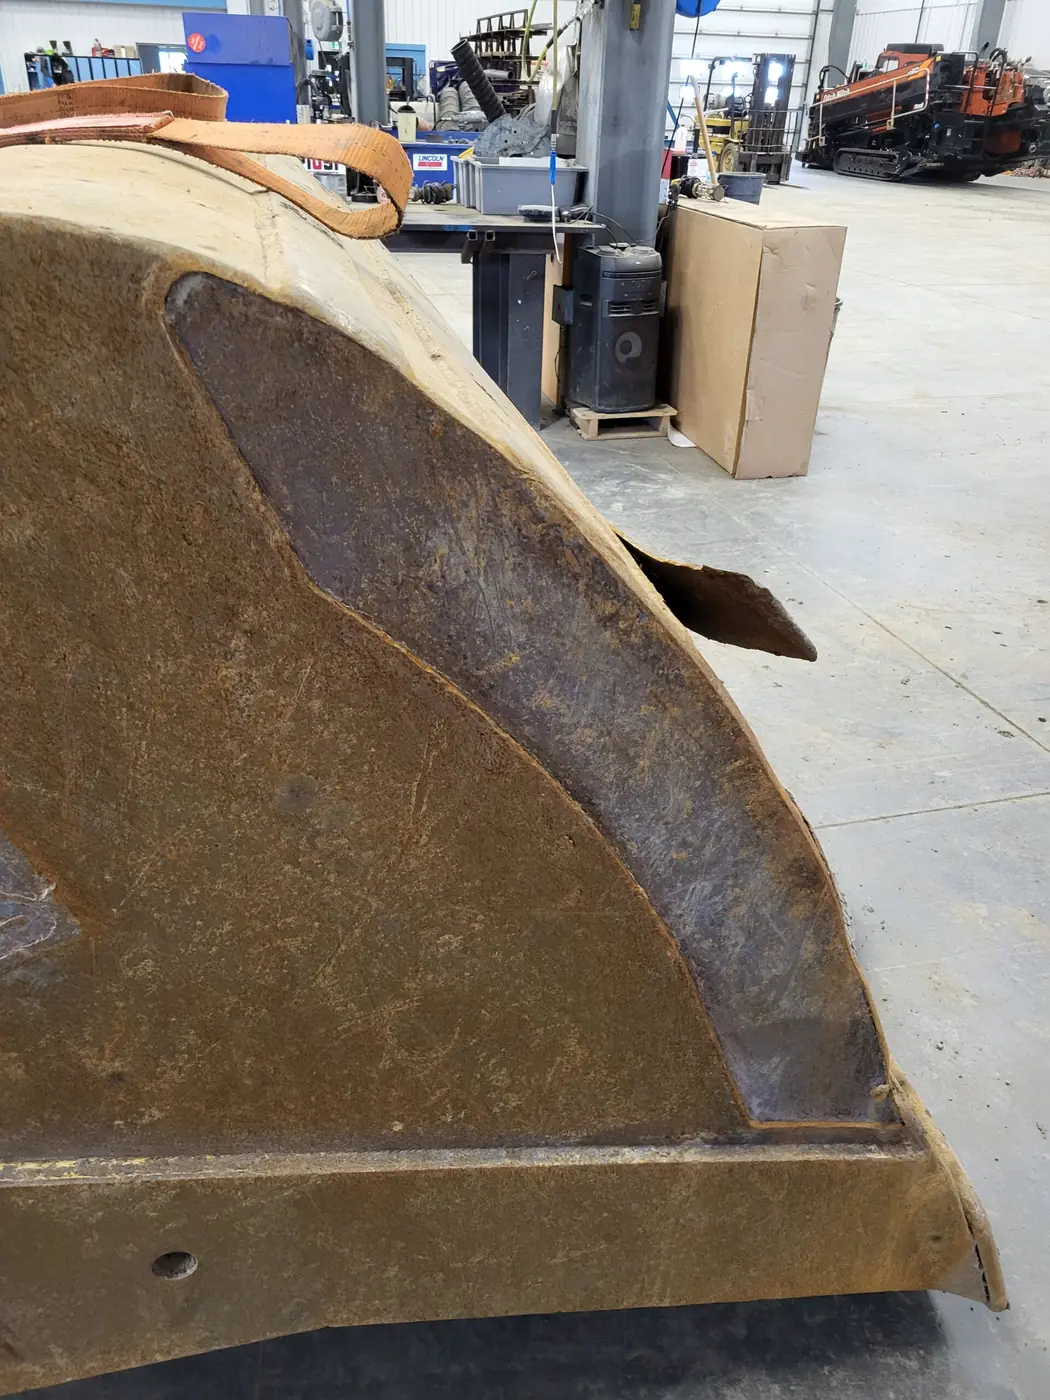
Worn excavator bucket side wall ready for repair

Repair or Replace a Bucket? How to Decide for Excavators and Loaders

Overview

A worn or damaged bucket leaves every equipment owner with the same question: is it worth fixing, or is it time for a new one? There isn’t one right answer for every bucket, but a few clear signs point the way. Here’s how to think it through before you spend money either direction.

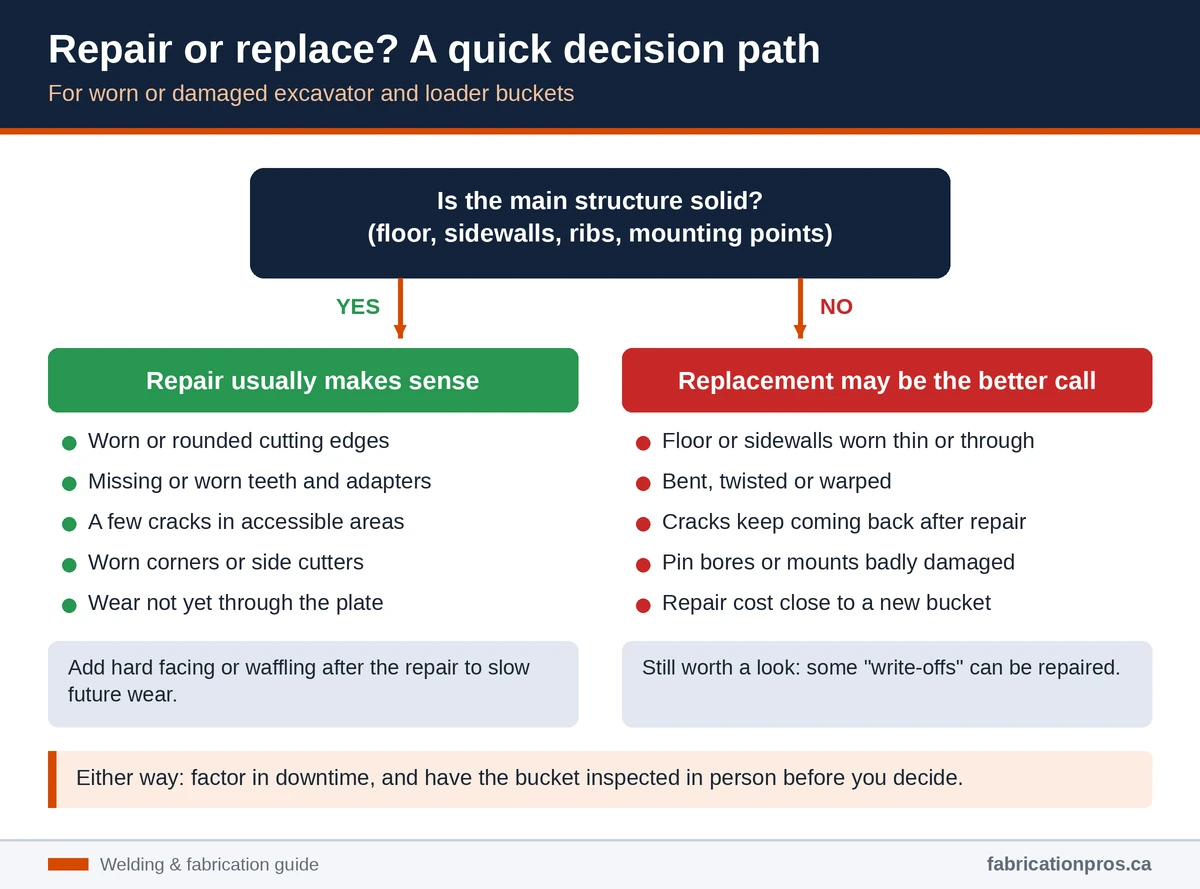
Start with the base metal

The bucket body is what you’re really paying for. Edges, teeth and cutters are designed to be replaced. If the main structure (floor, sidewalls, ribs and mounting points) is still solid, repair is usually on the table. If the structure itself is failing, the equation changes.

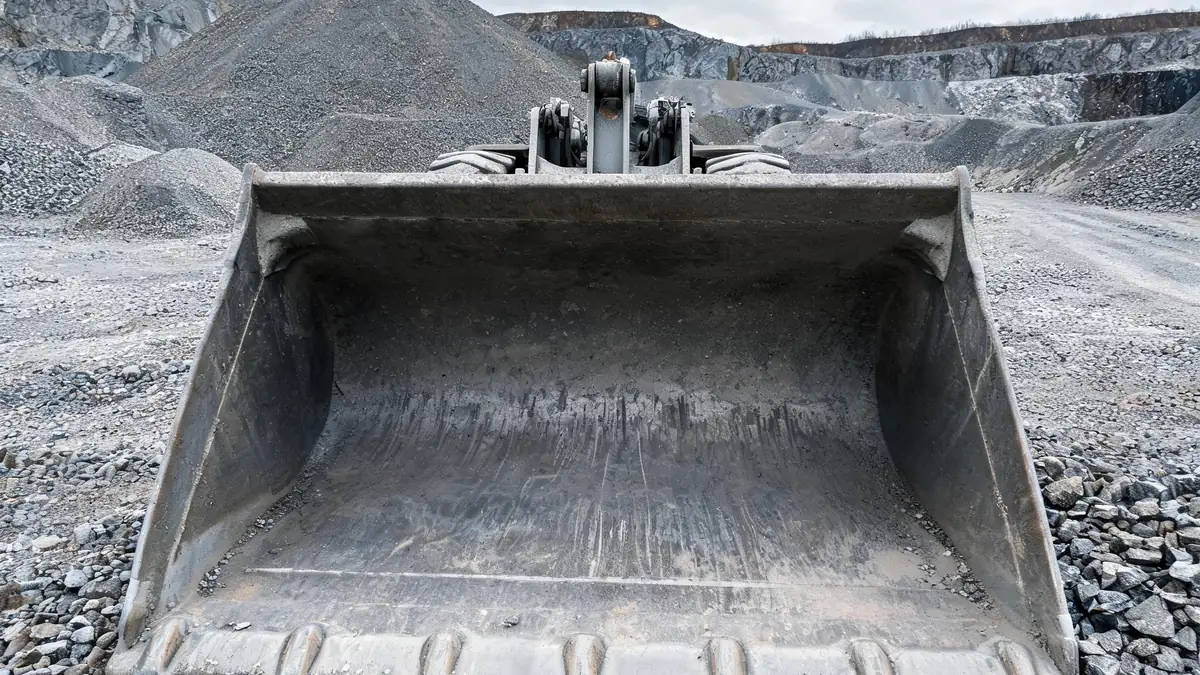
Worn wheel loader bucket with a rounded, thinned cutting edge and worn corners
A worn cutting edge and corners are wear parts; the real question is the condition of the floor, sidewalls and mounts.

Signs a bucket is usually worth repairing

  • Worn or rounded cutting edges
  • Missing or worn teeth and adapters
  • A few cracks in accessible areas
  • Worn corners or side cutters
  • Wear that hasn’t yet gone through the plate
  • Damage caught early

In these cases, repair often restores the bucket at a fraction of the cost of a new one, and protection such as hard facing or waffling can help keep it from wearing out again so quickly.

Signs replacement may be the better call

  • The floor or sidewalls are worn thin or through
  • The bucket is bent, twisted or warped
  • Cracks keep returning after repair
  • Mounting points or pin bores are badly damaged
  • Repair would cost close to the price of a replacement

Even then, it’s worth having a welder look at it. What looks like a write-off is sometimes repairable, and what looks fixable is sometimes a waste of money.

Flowchart for deciding whether to repair or replace an excavator or loader bucket based on the condition of the main structure
A quick way to frame the repair-or-replace decision before an inspection.

Questions to ask before you decide

  1. How much of the original steel is left?
  2. Is the damage in one area, or all over the bucket?
  3. How much would downtime cost you while you wait on a new bucket?
  4. What material are you digging, and will repair and protection hold up to it?
  5. How many hours of life does the machine itself have left?

Don’t forget downtime

Price isn’t the only cost. If a replacement has to be ordered and shipped, the machine sits idle. A repair on site can get you working sooner. Our mobile welding repair service travels to job sites in and around Calgary, so you may not have to haul the bucket anywhere.

The only reliable way to know

A photo can help, but an in-person inspection is the honest way to decide. We’ll look at the bucket, tell you what we see, and explain your options, whether that’s a repair, added protection or a replacement. Learn more about our heavy equipment welding and repair work, visit the Fabrication Pros homepage, or contact us for a free quote.

If your project goes beyond buckets, our planning guide to welding and fabrication services in Calgary explains which type of service fits your job and what to send for a quote.

Contact us with any questions you may have.

No file chosen

Read more
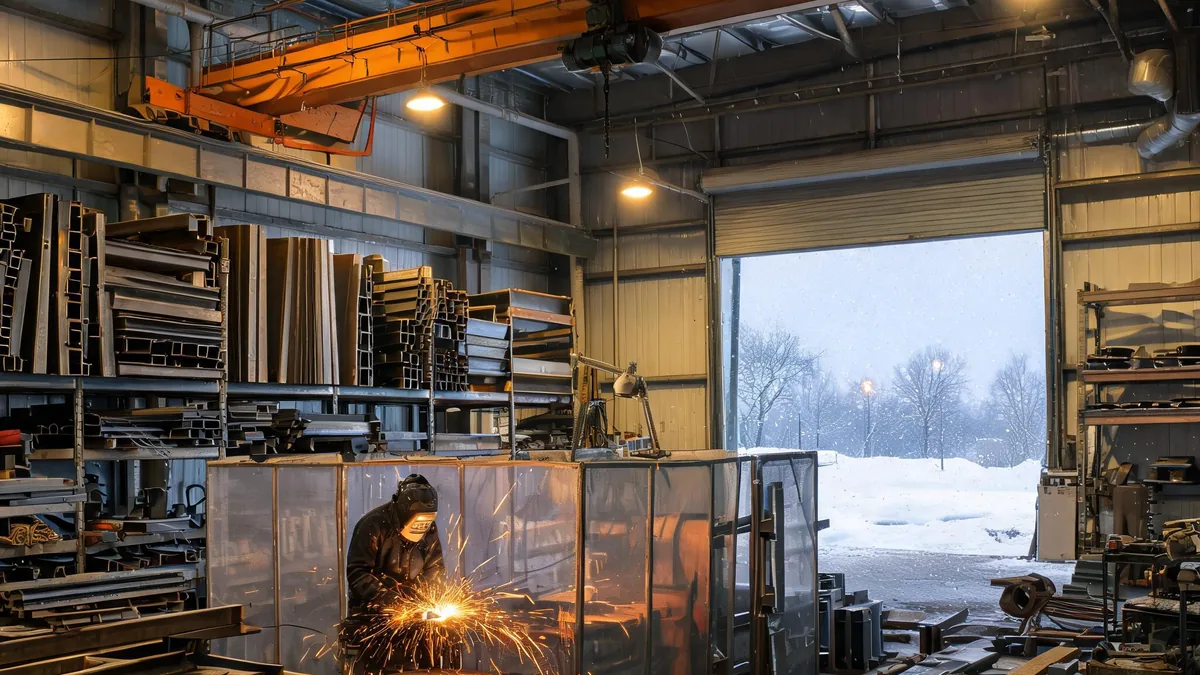
Metal fabrication shop with steel beams on racks, welding screens and a welder at work

Welding and Fabrication Services in Calgary: A Planning Guide

Overview

Most welding jobs start with a simple problem: something cracked, something wore out, or something needs to be built that you cannot buy off the shelf. The hard part is usually explaining the job so the right person can quote it properly. This guide walks through the main kinds of welding and fabrication work we do in Calgary and the surrounding area, how to tell which one your project falls under, and what information helps you get an accurate answer quickly.

Repair, fabrication or on-site work?

Nearly every request fits into one of three groups. Knowing which one you are in makes the first conversation much shorter.

  • Repairs restore something that already exists: a cracked trailer frame, a worn excavator bucket, a leaking aluminum tank or a broken bracket. The goal is to bring the part back to service, ideally stronger than before.
  • Fabrication means building something new from raw material, such as railings, stairs, gates, beams, skids or a custom part made to your drawing or measurements.
  • On-site work covers both repairs and installation when the item is too large, too heavy or too busy to bring to a shop. Equipment in the field, steel on a construction site and fixed structures usually fall here.

Common services and where to read more

The table below groups the work we handle by the type of job. Each link goes to a page with more detail on that service.

Type of jobTypical examplesLearn more
Mobile and on-site weldingField repairs, construction-site welding, emergency breakdownsMobile welding repair, portable welding services
Heavy equipmentExcavator and loader buckets, hard facing, waffling, structural cracksHeavy equipment welding and repair
Trailers and transportFrames, hitches, cross members, aluminum decksTrailer welding and repair
Aluminum and stainless steelRepairs and fabrication in non-ferrous and corrosion-resistant metalsAluminum welding, stainless steel welding
Fuel tanksCracked or leaking aluminum diesel tanksAluminum fuel tank repair
Pressure and industrialB pressure welding, process piping, pressure vessels, skid packagesB pressure welding, process piping, pressure vessels, skid packages
Oilfield and rig workWelding on and around drilling and service rigsRig welding services
Structural steelBeams, columns, trusses and new constructionStructural beam, column and truss fabrication, new construction welding
Custom metalworkRailings, stairs, ramps, gates and fencesCustom gates, railings and stairs

For the full list in one place, see our welding and fabrication services overview.

Which welding process does your job need?

You do not need to choose a welding process yourself, but it helps to know why a welder might recommend one over another. The main factors are the metal, its thickness, where the work happens and how the finished weld will be loaded.

  • MIG (GMAW) is fast and clean on steel, stainless and aluminum, and works best indoors. See what GMAW welding is.
  • TIG (GTAW) gives the most control on thin material, stainless and aluminum where appearance matters. Our GTAW TIG welding guide explains why.
  • Stick (SMAW) handles wind, dirty steel and thick sections well, which is why it is common for field repairs. Read the SMAW stick welding guide.
  • Flux-cored (FCAW) deposits a lot of metal quickly and is popular for structural and heavy equipment work. See our flux core arc welding guide.

Shop or on site?

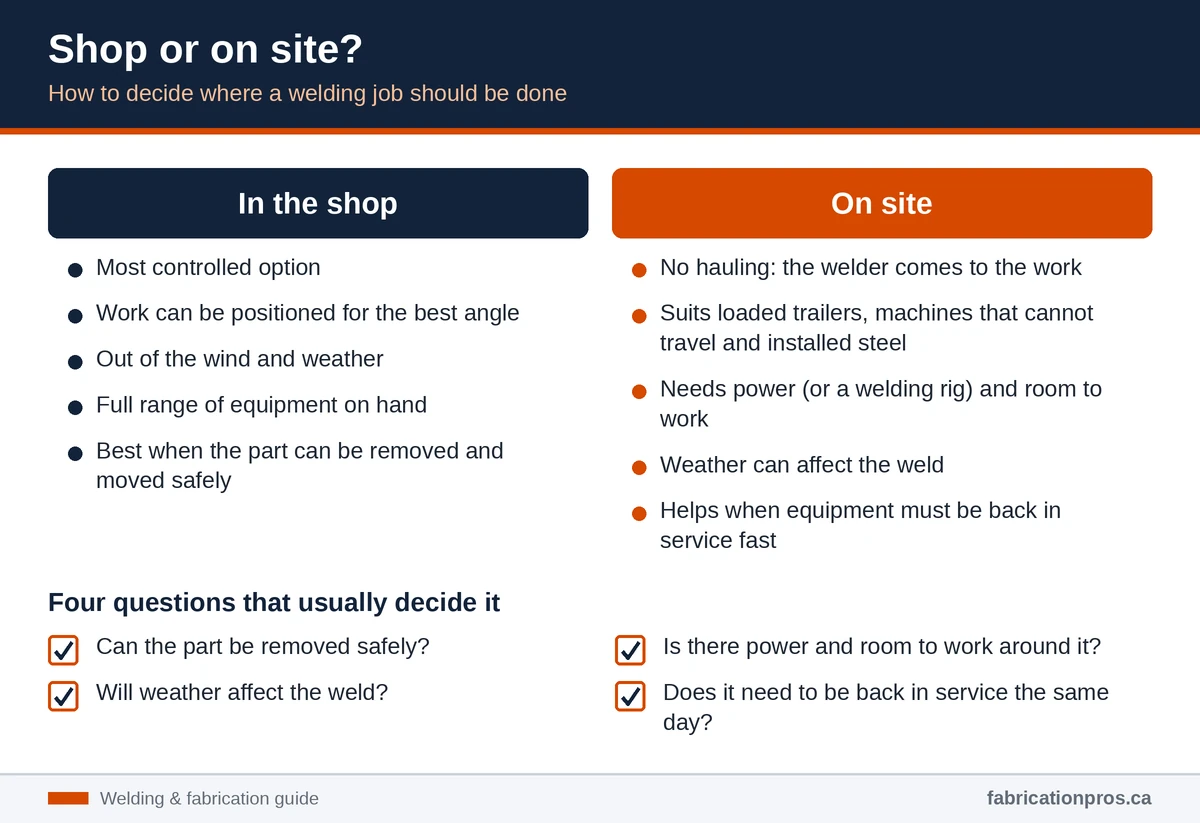
Bringing a part to the shop is usually the most controlled option. The welder can position the work for the best angle, keep it out of the wind and use the full range of equipment. On-site work makes more sense when moving the item would cost more time or money than the repair itself, for example a loaded trailer, a machine that cannot travel, or steel that is already installed.

A few questions decide it: Can the part be removed safely? Is there power and room to work around it? Will weather affect the weld? Does the equipment need to be back in service the same day? If you are not sure, describe the situation and we can suggest the better option.

Comparison of welding in the shop versus on site, with four questions that decide where the job is done
Where the work is done affects control, cost and turnaround.

What to send when you ask for a quote

A clear request saves a site visit in many cases. These details help us understand the job before anyone picks up a torch:

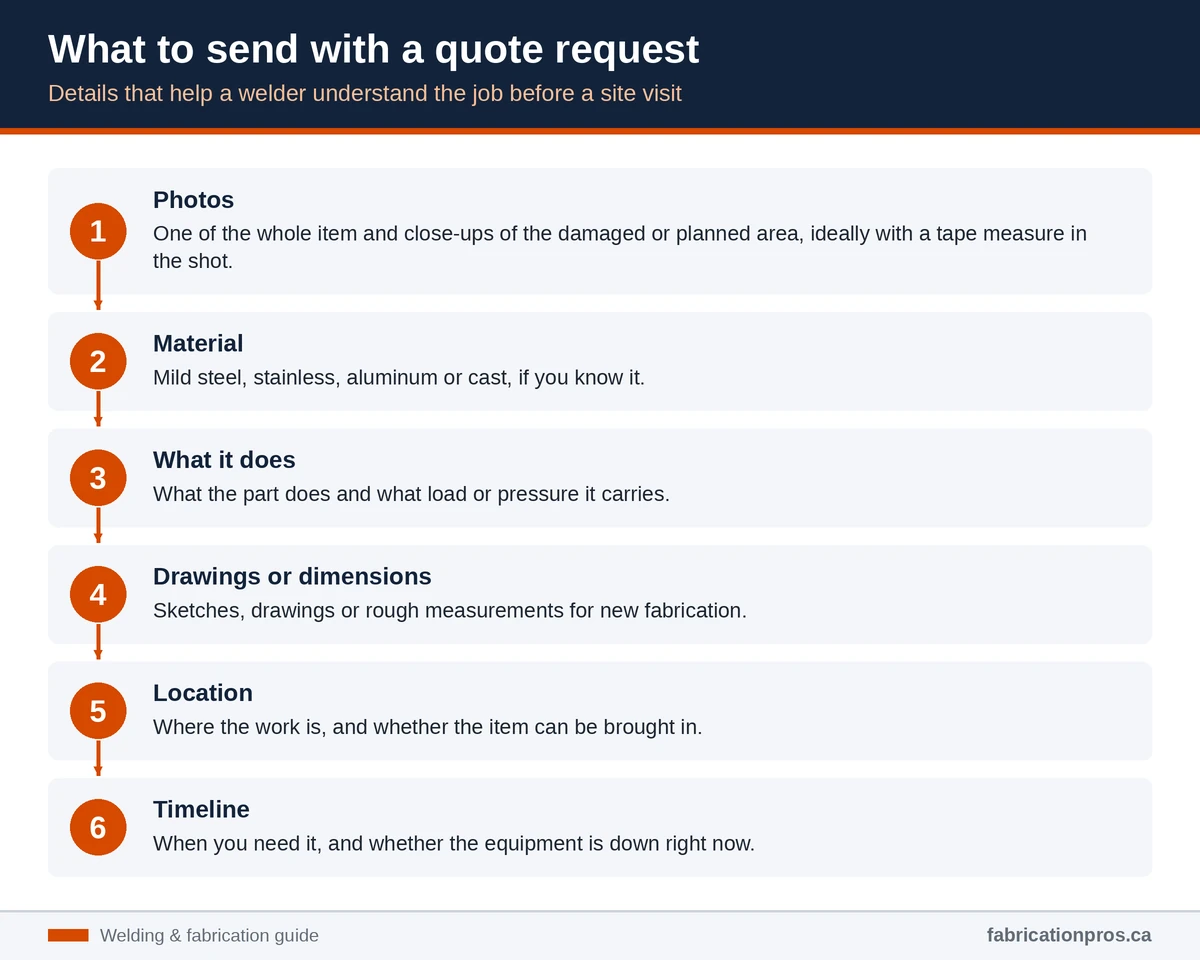
  • Several photos: one of the whole item and close-ups of the damaged or planned area, ideally with a tape measure in the shot
  • The material, if you know it (mild steel, stainless, aluminum or cast)
  • What the part does and what load or pressure it carries
  • Drawings, sketches or rough dimensions for new fabrication
  • Where the work is, and whether the item can be brought in
  • Your timeline, and whether the equipment is down right now
Checklist for a welding quote request: photos, material, what the part does, drawings, location and timeline
Six details that make a quote faster and more accurate.

Questions worth asking any welding shop

  1. Have you repaired or built this type of item before?
  2. Which process and filler metal do you plan to use, and why?
  3. Will the area be cleaned, ground or bevelled before welding?
  4. Does the job need any certification, inspection or documentation?
  5. Can the work be done in the shop, or does it need to be done on site?

A good welder will be happy to explain the plan in plain language. If a repair is not worth doing, they should tell you that too. Our article on whether to repair or replace a worn excavator bucket is a good example of how that decision is made.

Welding in a Calgary climate

Local conditions affect welding more than people expect. Cold steel pulls heat out of a weld quickly, so thicker parts often need preheating in winter to avoid cracking. Snow, frost and condensation have to be dried off the joint first. Road salt and gravel are hard on trailers and truck equipment, which is why spring is a common time to find cracked cross members and rusted mounts. Planning repairs before the busy construction season can also save waiting time.

Talk to us about your project

Whether you need a quick repair, a custom part or a crew on site, Fabrication Pros can help you figure out the next step. Visit the Fabrication Pros homepage to see more of our work, or contact us to request a quote.

Contact us with any questions you may have.

No file chosen

Read more