Aluminum and steel might look like they’d weld in much the same way. They don’t. Aluminum is lighter and resists rust, which is why it’s so common on trailers, fuel tanks, boats and food equipment, but it behaves very differently under a welding arc. Knowing why helps you understand what a good aluminum weld requires and why not every welder or shop does it well.
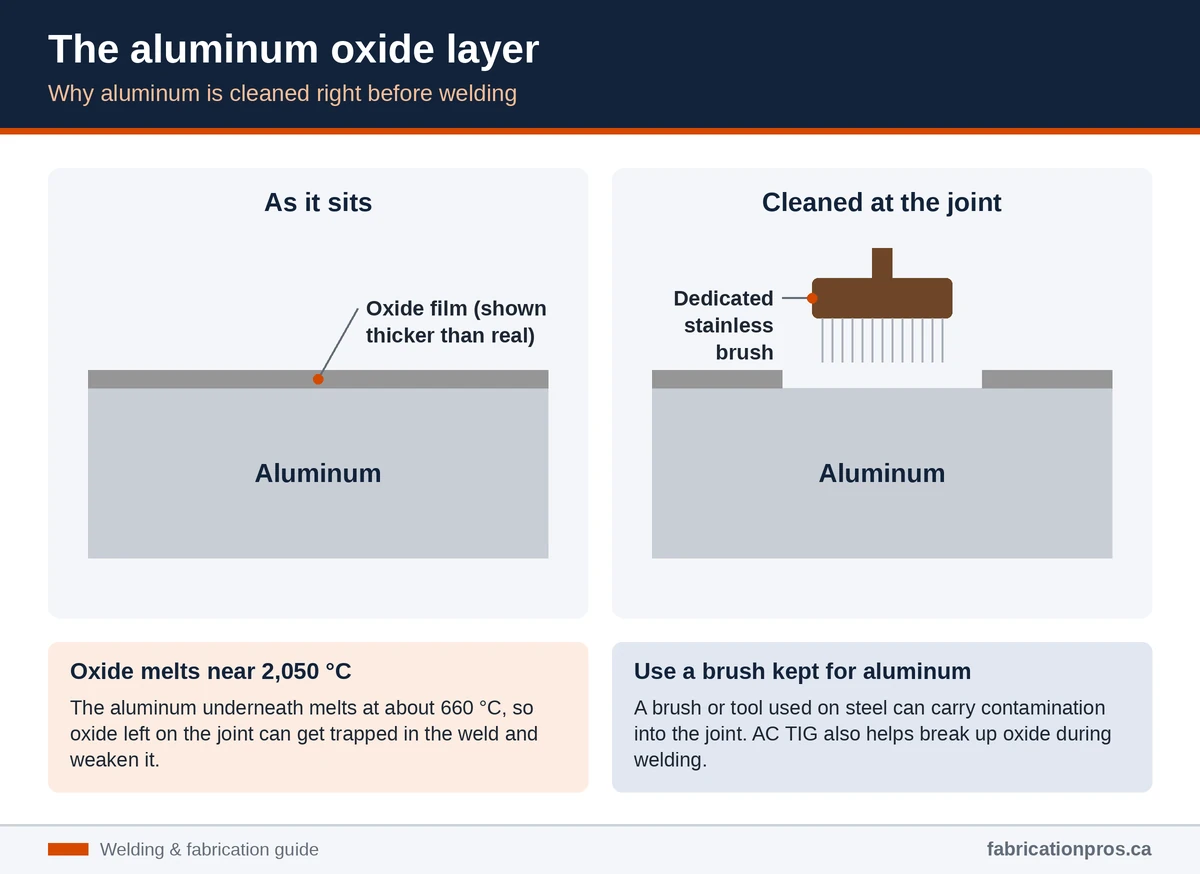
Aluminum forms a thin, tough oxide layer on its surface almost immediately. That layer melts at a much higher temperature than the aluminum underneath it. If the oxide isn’t removed before welding, it can get trapped in the weld and weaken it. That’s why aluminum has to be cleaned carefully before welding, using a dedicated stainless steel brush or other suitable cleaning method rather than a tool that’s been used on other metals.
The oxide skin melts at a far higher temperature than the aluminum under it.
Heat behaves differently
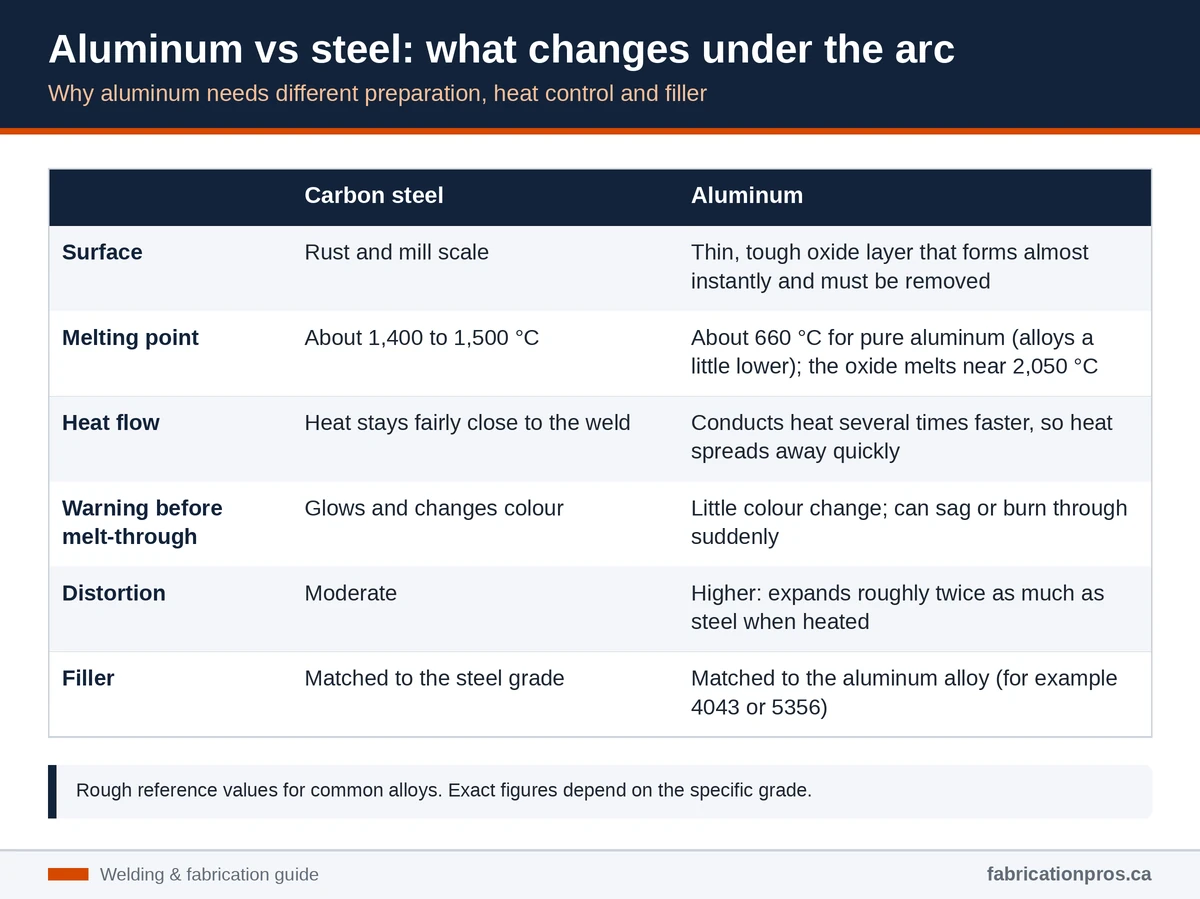
Aluminum conducts heat far better than steel. Heat spreads quickly away from the weld, so more heat input is often needed to get started. But aluminum also melts at a lower temperature than steel and gives little warning before it sags or burns through. Controlling heat is a big part of the skill, especially on thin material.
It’s softer and moves more
Aluminum expands more when heated than steel does, so parts can distort as they heat and cool. Careful fit-up, clamping and welding sequence help keep the finished piece straight. Because aluminum is softer, it’s also easier to damage while handling and preparing.
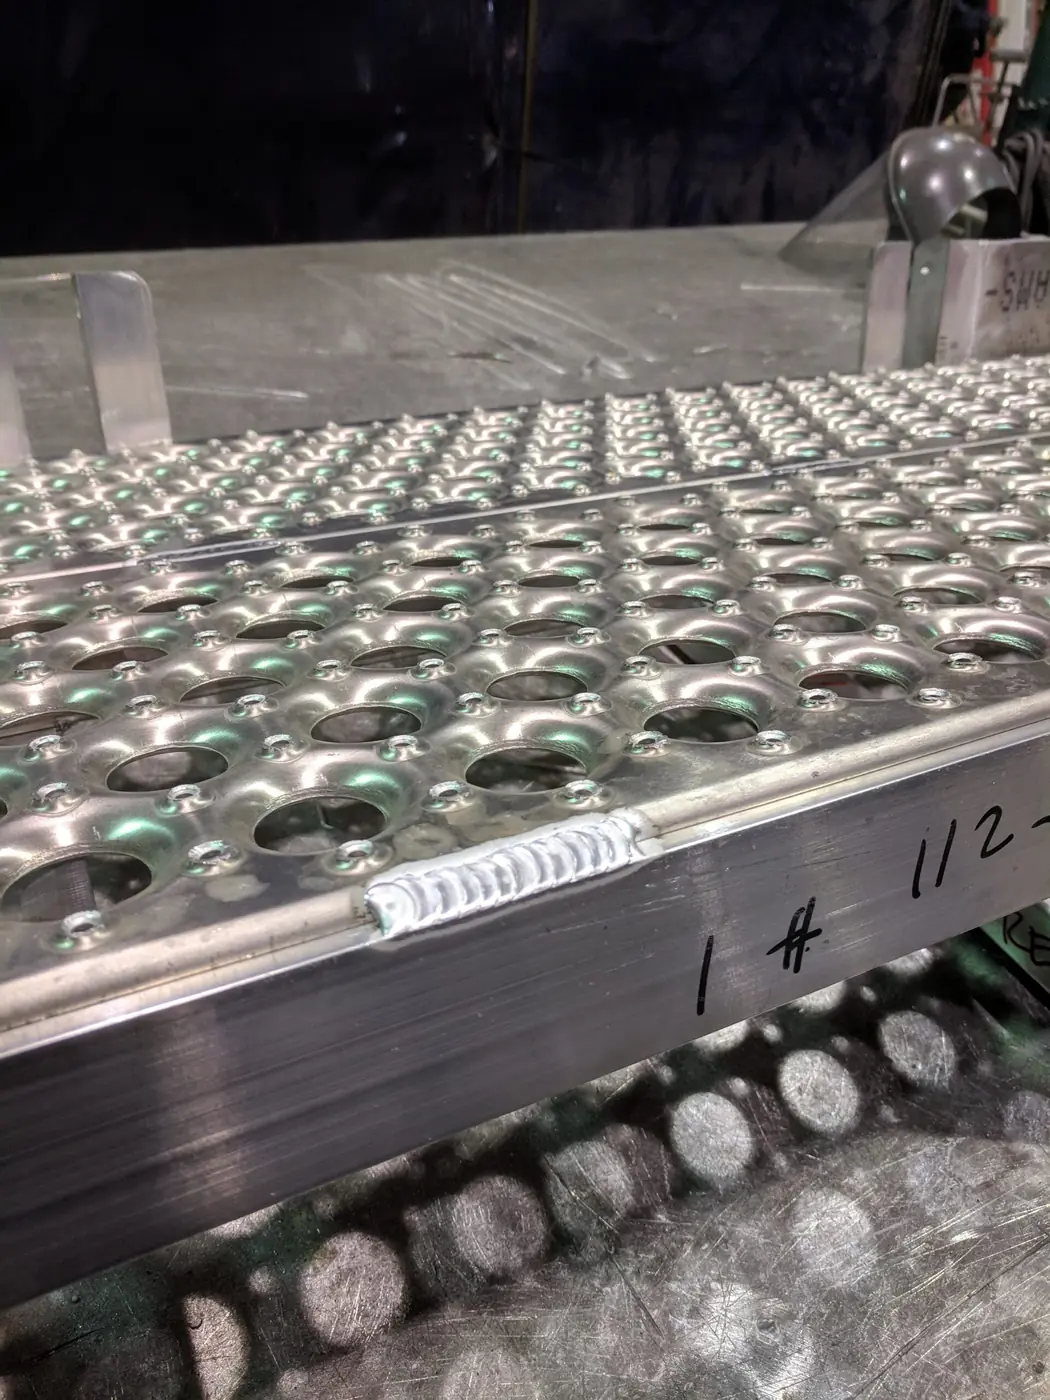
How aluminum differs from steel once the arc is on.
Filler metal matters
Different aluminum alloys need different filler metals, and the wrong choice can cause cracking or a weaker joint. We cover this in more detail in our post on the difference between aluminum filler alloys.
Welding processes for aluminum
Aluminum is commonly welded with TIG (GTAW) or MIG (GMAW), and each has its place. TIG gives fine control and is often chosen for thin material and visible, precise welds. MIG is faster and suits longer runs and thicker material. Learn more in our guide to TIG (GTAW) welding.
MIG Welding Tips and Tricks: A Complete Guide for Cleaner, Stronger Welds
Overview
MIG welding (Metal Inert Gas welding), also known as GMAW, is one of the most popular welding processes thanks to its speed, ease of use, and versatility. Whether you’re a beginner learning the basics or an experienced welder looking to refine your technique, mastering a few key MIG welding tips and tricks can dramatically improve weld quality, penetration, and overall efficiency.
In this guide, we’ll break down practical, real-world advice to help you get better results every time you strike an arc.
MIG welding uses a continuously fed wire electrode and a shielding gas to protect the weld pool from contamination. It’s commonly used on mild steel, stainless steel, and aluminum, making it a go-to process for automotive, fabrication, manufacturing, and DIY projects.
1. Choose the Right Wire and Gas Combination
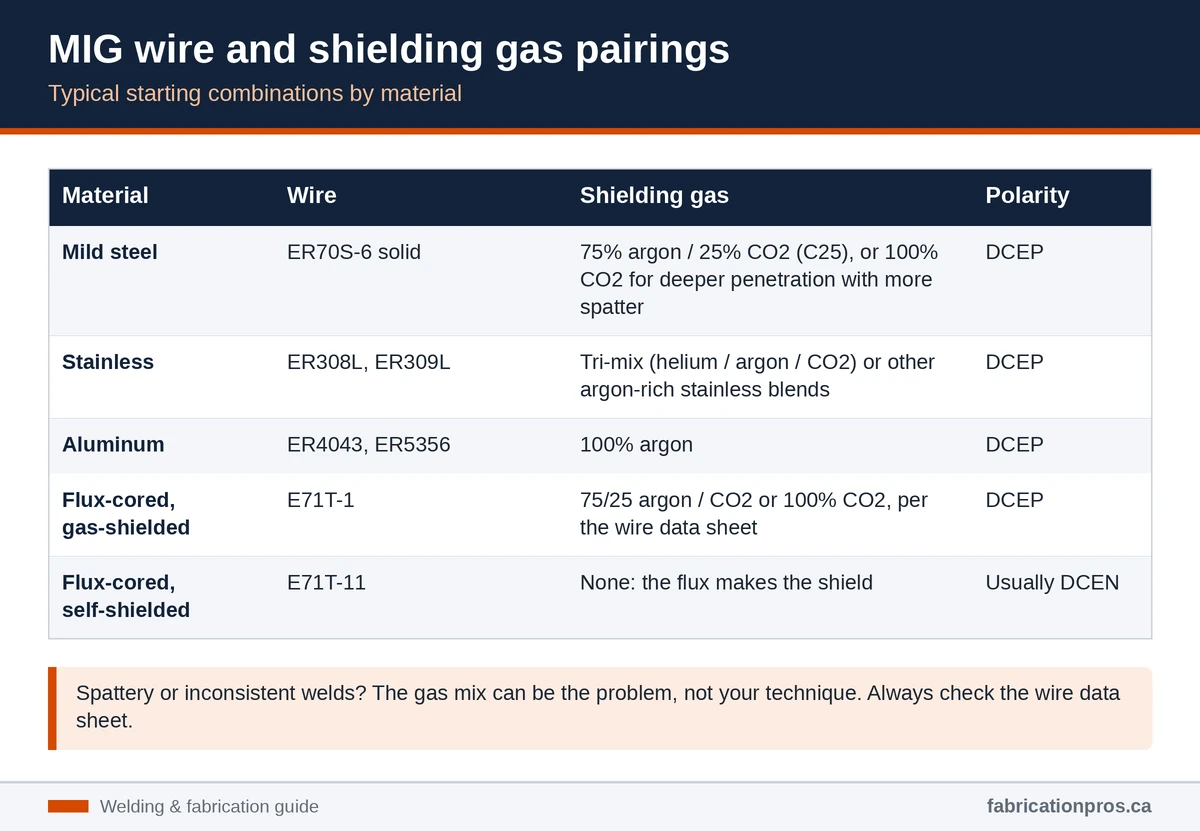
One of the most overlooked MIG welding tips is matching the wire type with the correct shielding gas.
MIG welding is forgiving, but precision separates average welds from great ones. By applying these MIG welding tips and tricks, you’ll see immediate improvements in bead appearance, penetration, and overall weld quality.
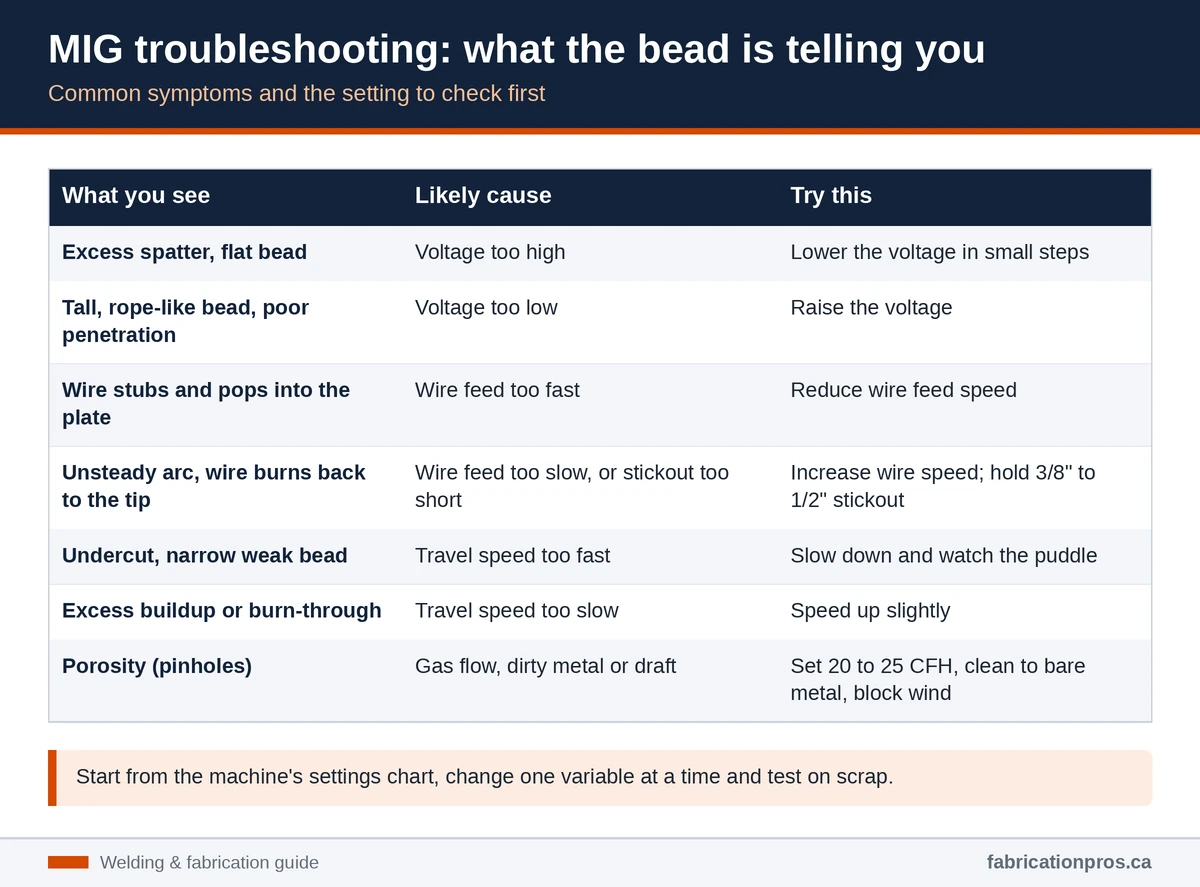
The real secret? 👉 Practice on scrap, adjust one variable at a time, and pay attention to the puddle.
In Calgary’s industrial, construction, and repair sectors, few welding processes are as reliable and versatile as SMAW—Shielded Metal Arc Welding, commonly known as stick welding. Whether you’re working on heavy equipment, structural steel, pipelines, farm machinery, or on-site repairs in difficult conditions, SMAW remains one of the most trusted welding methods in Alberta.
This comprehensive guide explores how SMAW works, best practices for strong structural welds, the most common electrode types, polarity differences, and where stick welding is used across Calgary’s residential, commercial, and industrial markets.
SMAW (Shielded Metal Arc Welding) is a manual welding process that uses a flux-coated consumable electrode, commonly called a “stick rod.” When the rod strikes the metal, it creates an electric arc that melts both the base metal and the electrode, forming a strong weld pool.
The key advantage of SMAW is that it does not require external shielding gas. Instead, the electrode’s flux coating releases gases and forms a protective slag that shields the weld from atmospheric contamination.
This makes stick welding extremely useful in locations where MIG or TIG welding cannot be used, such as:
Outdoor worksites
Windy conditions
Dirty environments
Remote areas
Industrial shutdown work
Why Stick Welding Is So Popular
Calgary’s diverse industries—including oil & gas, construction, heavy equipment, agricultural operations, manufacturing, and fabrication shops—rely heavily on SMAW because of its:
✔ Versatility
Works on steel, cast iron, stainless steel, hardfacing, pipelines, and heavy structural components.
✔ Portability
Only requires a welding machine and rods—no gas cylinders, hoses, or wire feeders.
✔ Performance Outdoors
Handles wind, moisture, and dirt much better than TIG or MIG.
✔ Deep Penetration
Many SMAW electrodes deliver strong, structural-grade penetration ideal for heavy steel.
✔ Cost-Efficiency
Equipment setup is simple, inexpensive, and easy to maintain.
How SMAW (Stick Welding) Works
Stick welding is simple in concept but requires skill, technique, and electrode knowledge to master. Here’s how the SMAW process works:
1. Power Source & Polarity
SMAW uses either:
AC (alternating current)
DCEP (direct current electrode positive)
DCEN (direct current electrode negative)
Electrode type determines the correct polarity. Rods like 7018 typically use DCEP, while rods like 6013 and 6011 may use AC or DC.
Correct polarity affects:
Arc stability
Penetration
Weld bead appearance
Spatter levels
2. Striking the Arc
The welder starts the arc using:
A tap technique, or
A scratch technique (like striking a match)
Once the arc starts, the rod and base metal melt into a controlled weld puddle.
3. Flux Coating Activation
The flux coating burns and produces:
Shielding gas → protects molten metal
Slag layer → solidifies on top of the weld
Arc stabilizers → regulate arc performance
Alloying elements → improve weld metal strength
This self-shielding feature is what makes SMAW ideal for outdoor and remote locations.
4. Weld Pool Formation
As the rod melts, it adds filler metal to the joint. The welder controls:
Rod angle
Travel speed
Arc length
Heat input
Puddle size
Proper technique creates a smooth, strong weld.
5. Slag Removal
Once the weld cools slightly, the slag is removed with:
A chipping hammer
A wire brush
Removing slag reveals the finished bead and prepares the surface for additional weld passes.
Best Practices for Strong, Clean SMAW Welds
Professional welders follow strict techniques to ensure structural integrity and aesthetic weld quality:
🔧 Maintain the right arc length
Too long → spatter, undercut, porosity Too short → sticking, unstable arc
🔧 Use the correct rod angle
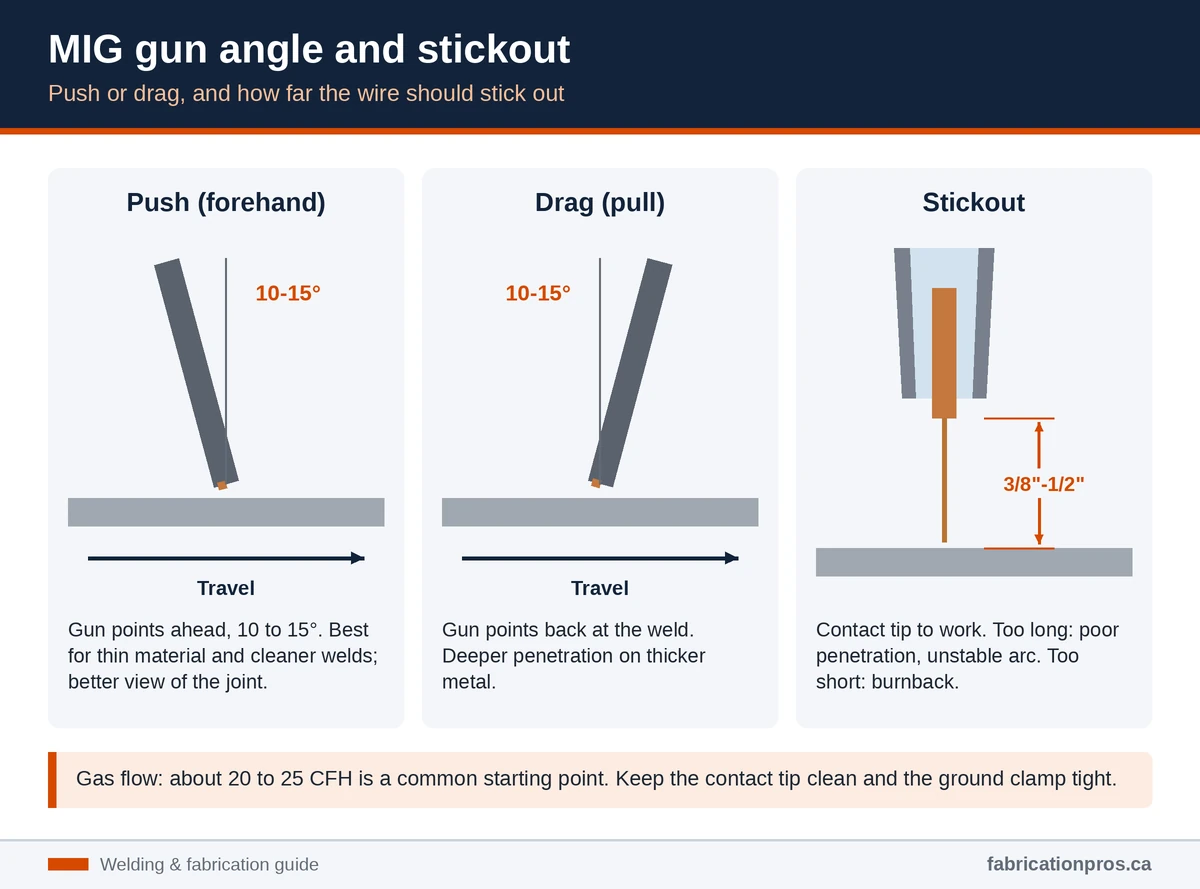
Typically 10–15° drag angle depending on joint type.
🔧 Control travel speed
Slow = excessive buildup Fast = poor penetration
🔧 Keep electrodes dry
Moisture causes porosity and hydrogen cracking. Rods like 7018 should be stored in a rod oven.
🔧 Prep the metal properly
Although SMAW tolerates dirt better than TIG/MIG, cleaner metal always results in stronger welds.
🔧 Match amperage to the rod diameter
Example amperage ranges:
1/8″ 7018: 90–140 amps
1/8″ 6010: 70–120 amps
Common SMAW Electrode Types and Their Applications
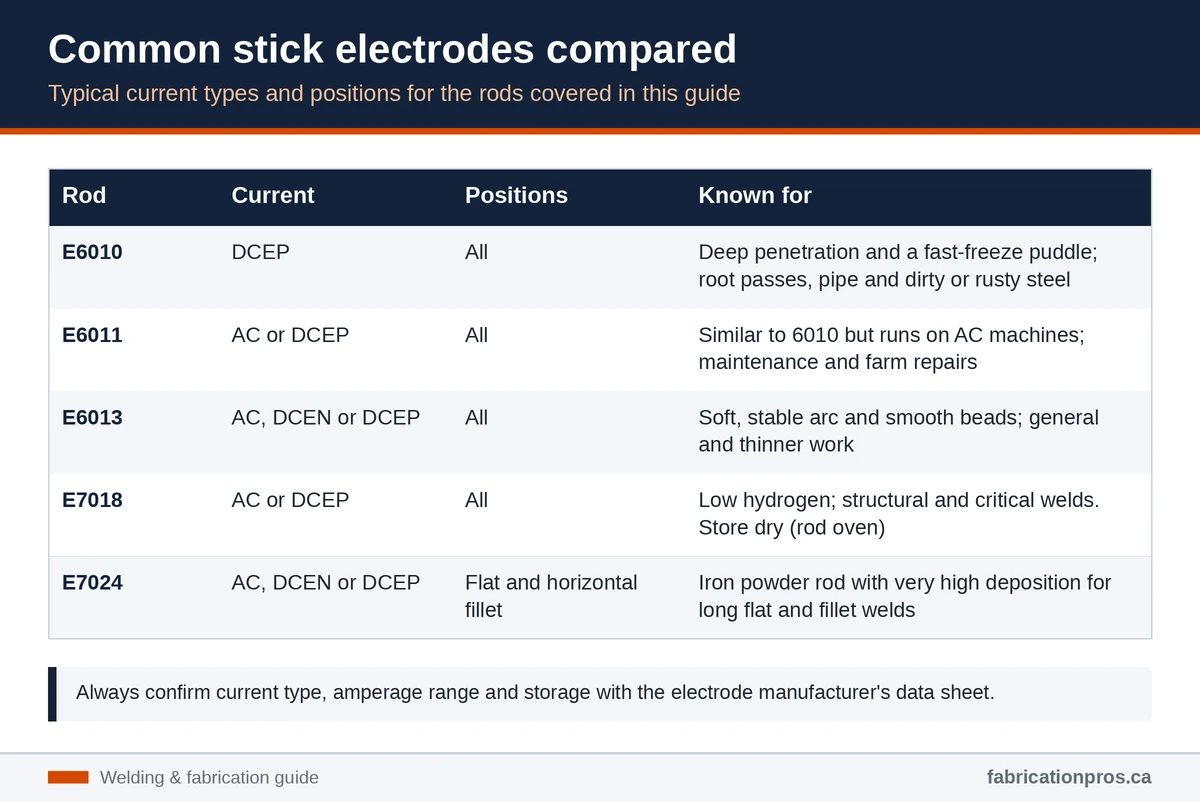
SMAW rods vary widely in performance. Here are the most common electrodes used in Calgary fabrication and repair work:
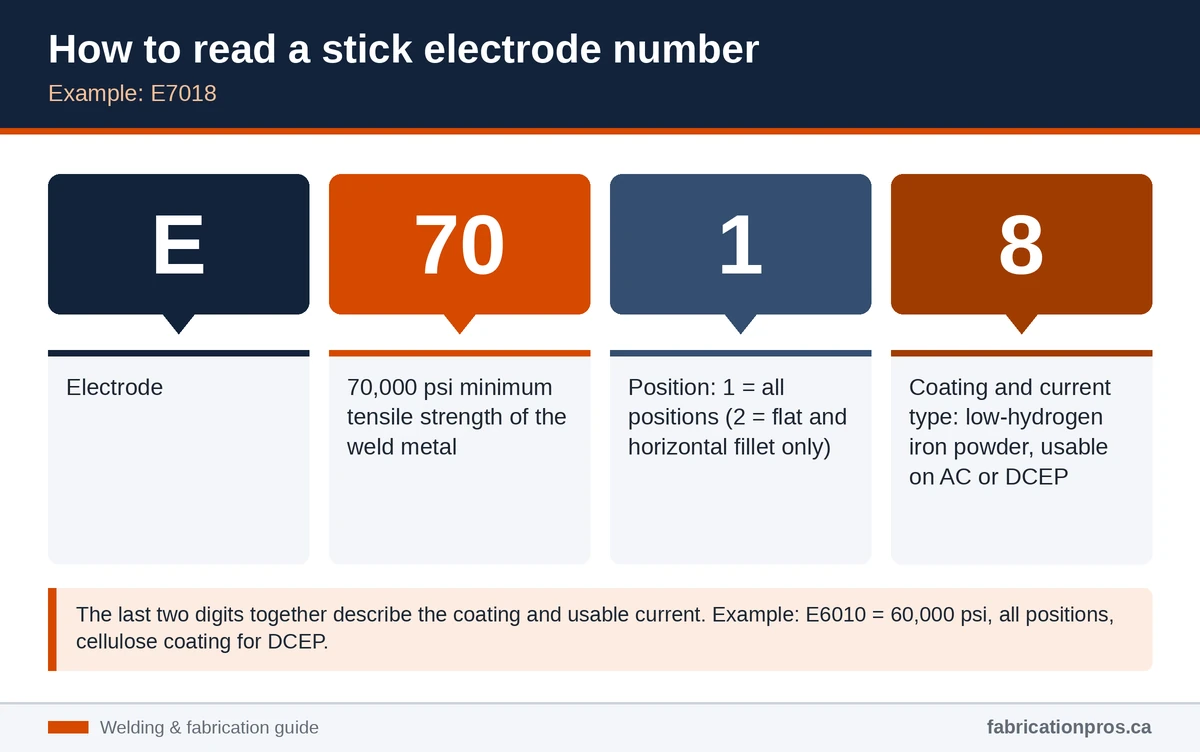
Every stick electrode number follows the same pattern.
E6010 – Deep Penetrating Pipe & Root Pass Rod
Good for:
Root passes
Pipeline welding
Dirty, rusty metal
Out-of-position welding
Advantages:
Fast-freeze puddle
High penetration
Great for vertical and overhead
E6011 – AC-Compatible Version of 6010
Good for:
Farm equipment
Maintenance welding
Sheet metal repairs
AC welders
Advantages:
Works on AC machines
Good for beginners
Great on dirty steel
E6013 – Smooth, Clean Beads
Common uses:
General fabrication
Thin metal
Fencing
Automotive sheet metal
Advantages:
Soft, stable arc
Minimal spatter
Cleaner weld appearance
E7018 – Low Hydrogen Structural Rod
The most popular rod in Calgary construction. Used for:
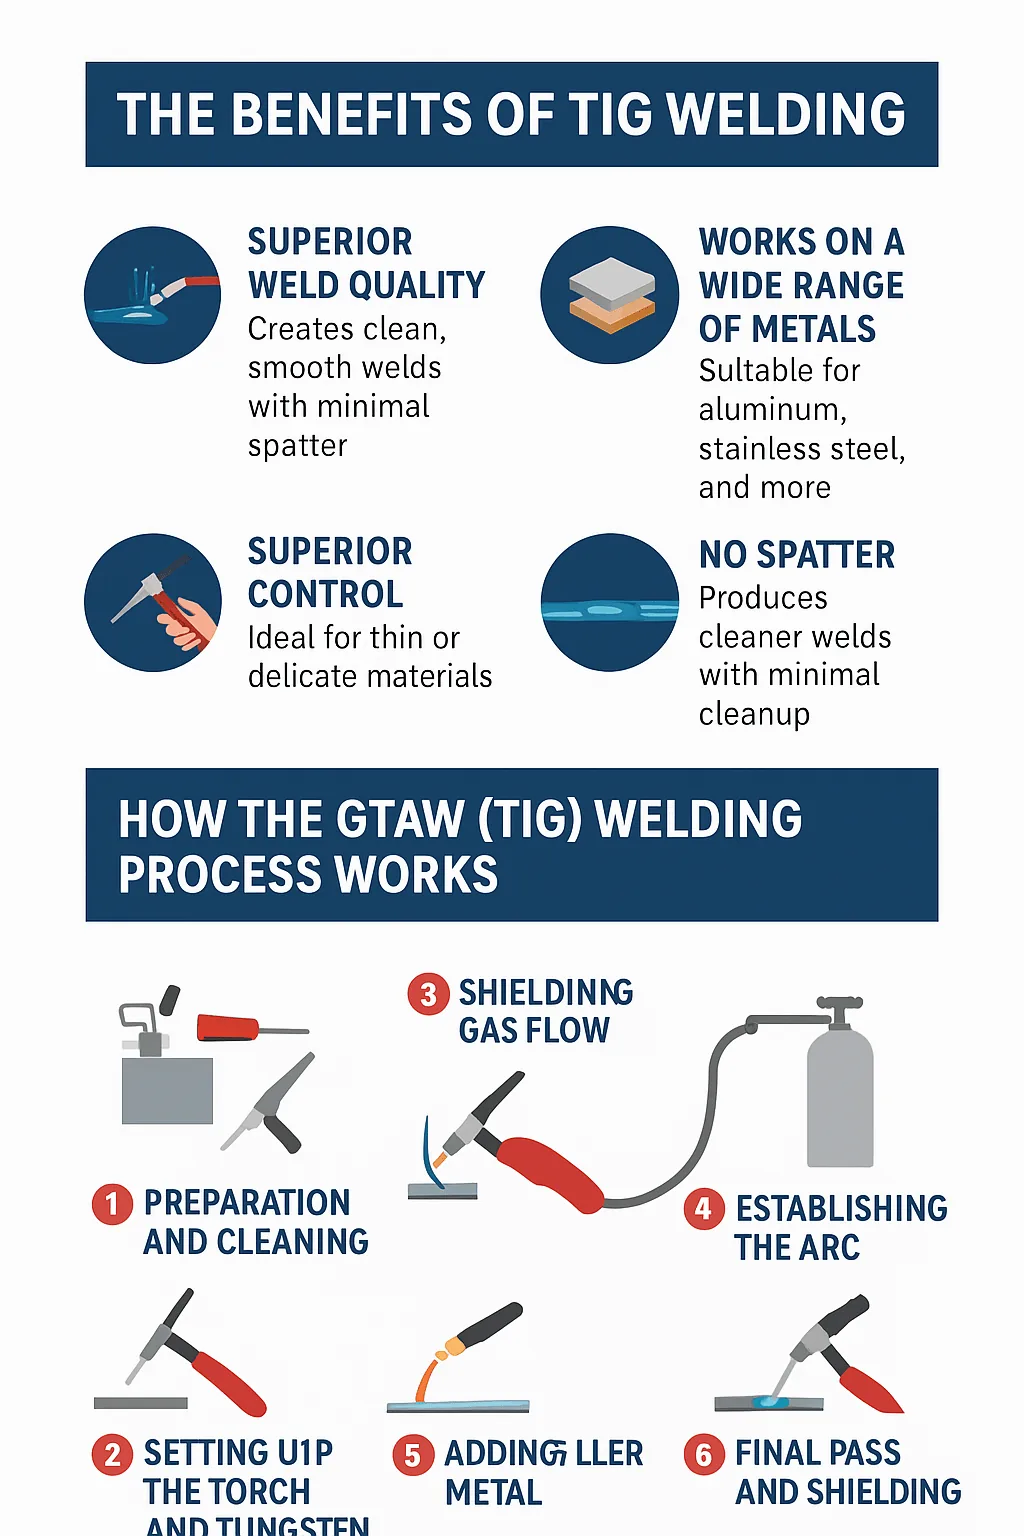
When precision, strength, and clean weld aesthetics matter, few welding processes compare to TIG welding, also known as GTAW (Gas Tungsten Arc Welding). At Fabrication Pros here in Calgary, Alberta, TIG welding is one of the core services we provide for residential, commercial, and industrial clients. From aluminum repairs to stainless steel fabrication, TIG welding delivers unmatched quality — and our certified welders use it daily on projects requiring the highest level of craftsmanship.
In this guide, we’ll break down the benefits of TIG welding and explain the GTAW process step-by-step, so you understand exactly why this method is trusted across Alberta’s industries.
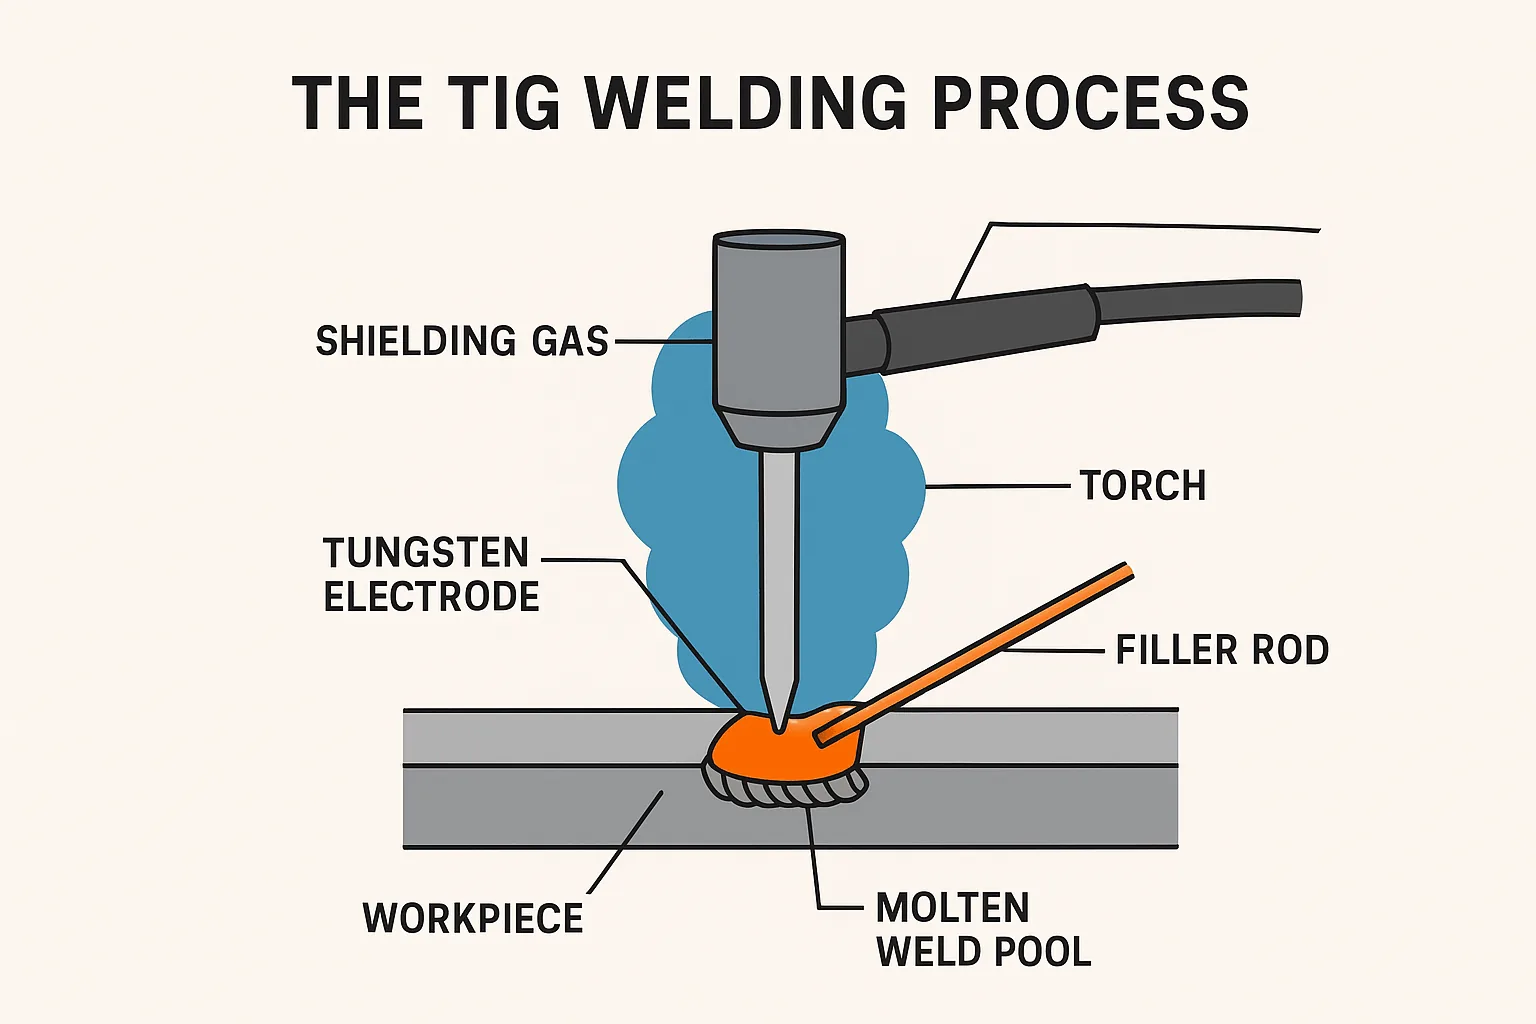
TIG welding basics, or Gas Tungsten Arc Welding, is a process that uses a non-consumable tungsten electrode to create an arc that melts the base metal. Instead of the electrode melting (like in MIG or stick welding), the welder controls the weld puddle and adds filler metal manually when needed.
A shielding gas — most commonly argon — protects the weld area from contamination and oxidation.
Because of this high level of control, TIG welding produces the cleanest, strongest, and most precise welds in the industry.
This flexibility allows our Calgary welding shop to take on everything from industrial repairs to automotive parts, brewery equipment, and custom fabrication.
3. Superior Control for Thin or Delicate Material
Unlike MIG or Stick welding, which can easily burn through thin metal, TIG is ideal for precision applications. Our welders can create strong welds on thin aluminum, stainless steel tubing, or lightweight components without distortion.
4. No Spatter and Minimal Cleanup
Because filler metal is added manually and the electrode doesn’t melt, TIG welding produces:
Zero slag
Zero spatter
Minimal cleanup
Cleaner finishes for painted or polished surfaces
In decorative or food-grade applications, this is a major advantage.
5. Stronger, More Reliable Welds
TIG welding is known for producing:
Deep penetration
Strong fusion
Consistent structural integrity
This is why industries like aerospace, oil and gas, agriculture, transportation, manufacturing, and construction rely heavily on the TIG process.
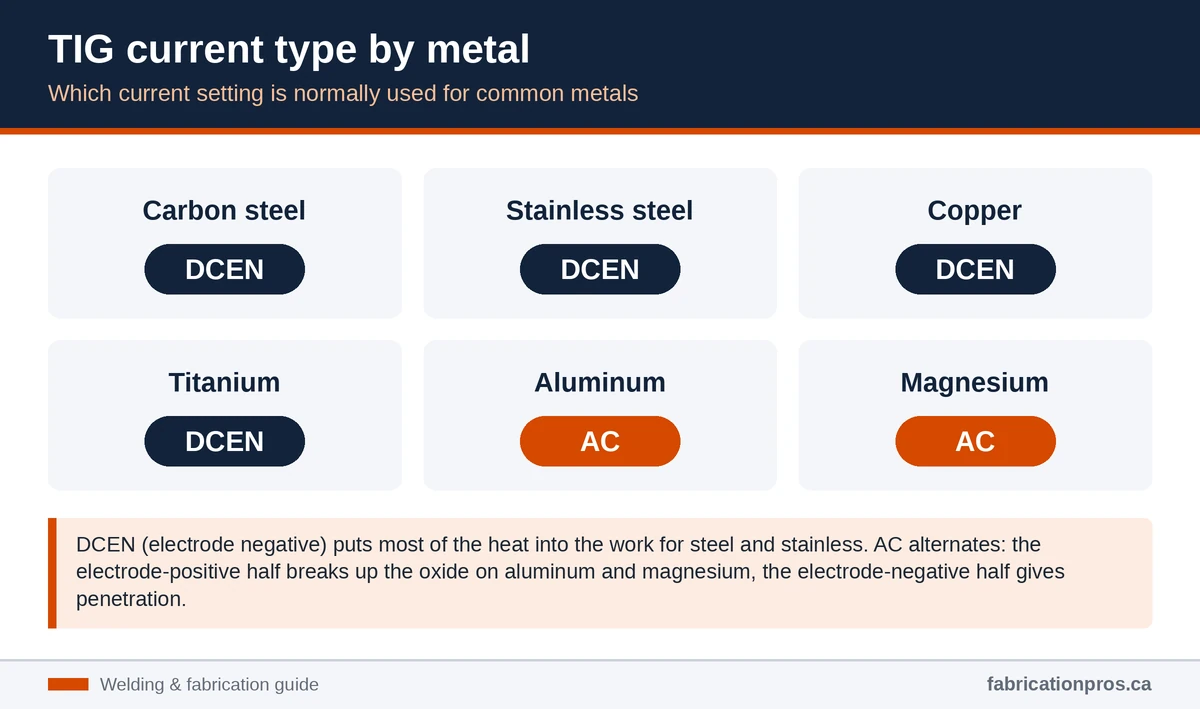
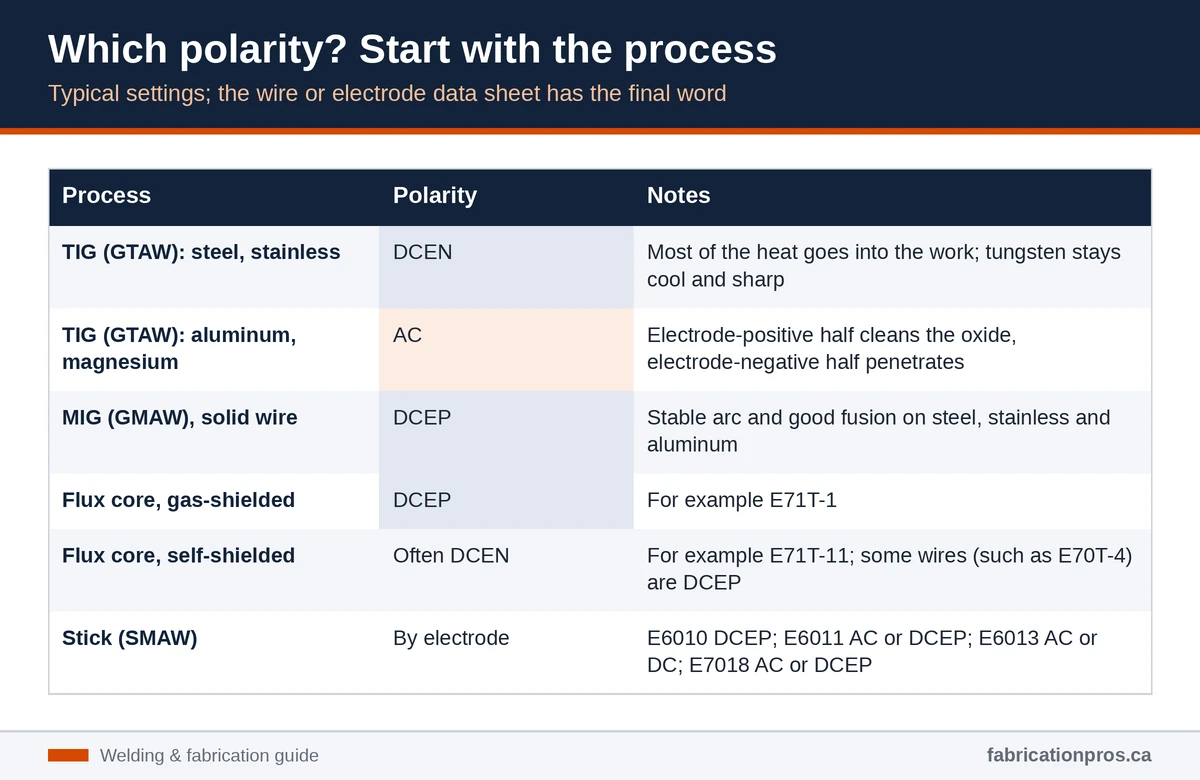
Steel and stainless run on DCEN; aluminum and magnesium need AC.
How the GTAW (TIG) Welding Process Works: Step-by-Step
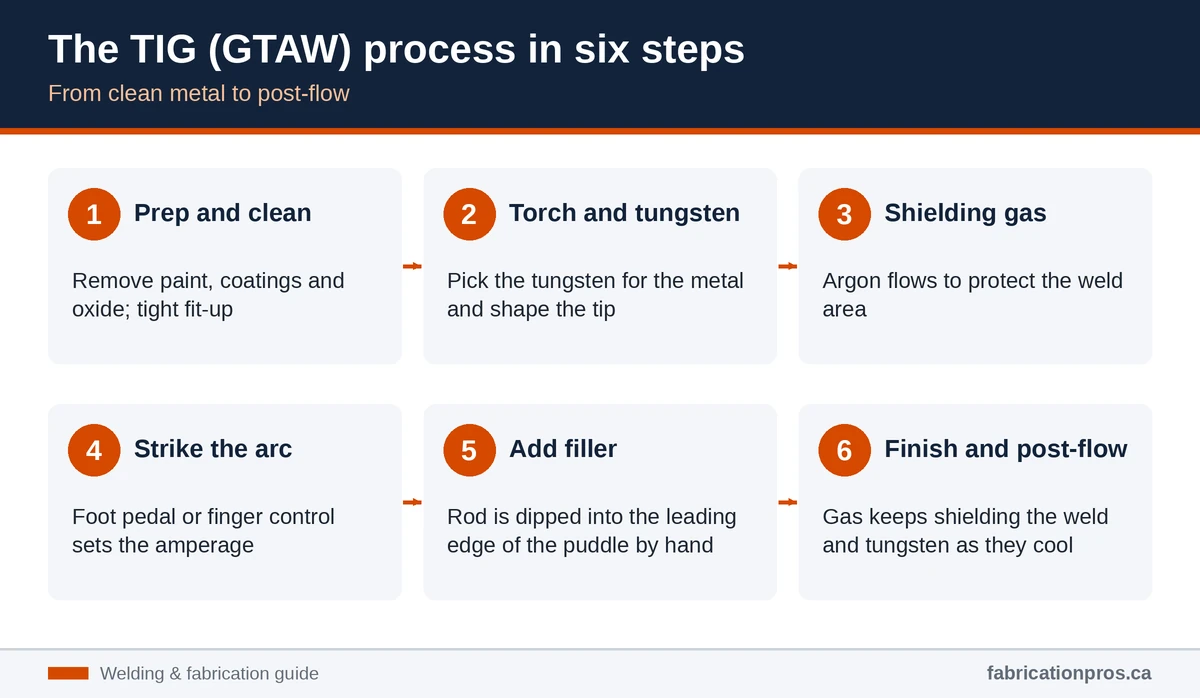
Below is the simplified breakdown of how our certified Calgary welders perform TIG welding in our shop and on mobile service calls:
1. Preparation and Cleaning
TIG welding requires extremely clean material. We prep the metal by:
Removing paint, coatings, or oxidation
Cleaning with acetone
Brushing aluminum with a stainless wire brush
Ensuring tight fit-ups
Clean metal = clean welds.
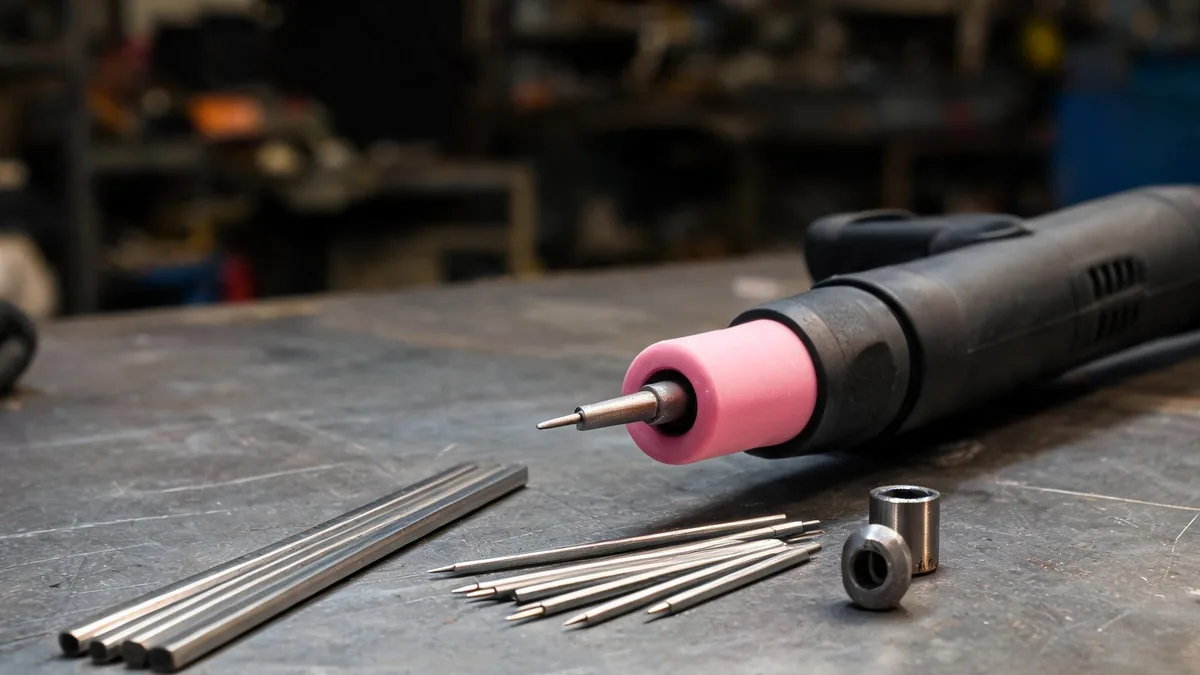
2. Setting Up the Torch and Tungsten
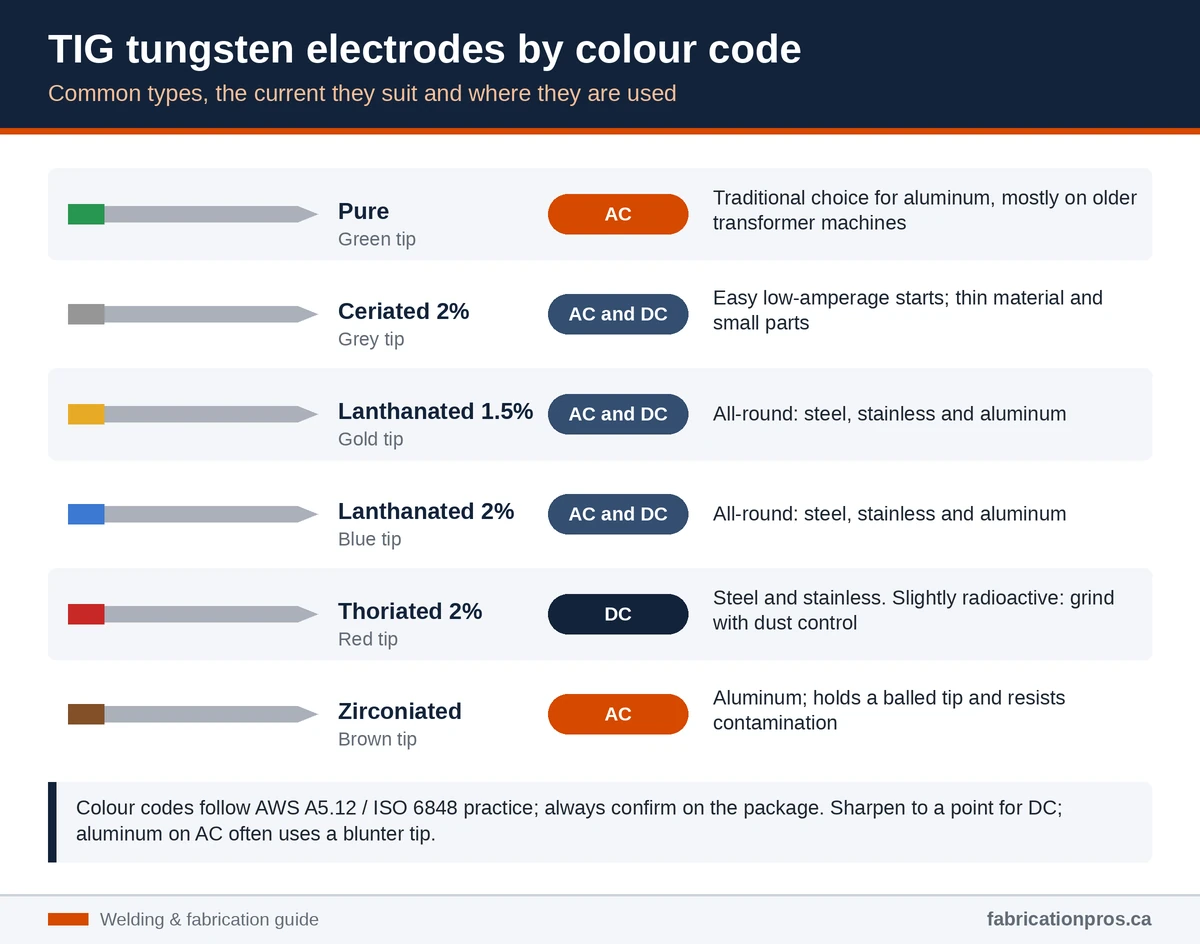
We choose the correct tungsten type based on the metal:
Red (Thoriated) – for steel and stainless
Green (Pure) or Blue/Gold (Lanthanated) – for aluminum
The tungsten is sharpened to a fine point for precision arc control.
3. Shielding Gas Flow
Pure argon gas is used to shield the weld area. This prevents:
Porosity
Contamination
Oxidation
For aluminum, argon provides smooth, stable arc performance.
4. Establishing the Arc
The welder uses a foot pedal or finger control to:
Start the arc
Control amperage
Maintain a stable puddle
This precise control is one of the biggest strengths of GTAW.
5. Adding Filler Metal
If additional metal is needed, filler rod is dipped into the puddle by hand. This allows:
Exact control over bead profile
Smooth transitions
Stronger welds
Common filler rods include ER4043, ER5356, ER70S-2, and stainless grades depending on the application.
6. Final Pass and Shielding
After the weld is complete, the torch continues shielding the weld until it cools slightly. This prevents:
Weld discoloration
Shielding gas turbulence
Structural weaknesses
Proper post-flow is essential for strong TIG welds.
The six stages of a TIG weld, from clean metal to post-flow.
Our team provides professional TIG/GTAW welding services in-shop or on-site. If you need clean, precise, and reliable welds, we’re the welding company Calgary businesses trust.
📞 Call us at (403) 879-3443 📍 Serving Calgary, Airdrie, Okotoks, Cochrane & surrounding Alberta 🌐 Contact Us for a free quote
When it comes to achieving clean, precise, and high-quality welds, GTAW welding—also known as TIG welding—stands at the top of the welding industry. For Calgary businesses that demand exceptional craftsmanship, from stainless steel fabrication to aluminum welding repairs, TIG welding is often the preferred solution. Whether you’re a facility manager, contractor, or industrial shop owner, understanding the benefits and process of TIG welding can help you choose the right welding service for your project.
This guide breaks down what GTAW/TIG welding is, how it works, best practices, filler wire types, and where it is most commonly used across Calgary’s residential, commercial, and industrial sectors.
GTAW stands for Gas Tungsten Arc Welding, often referred to as TIG welding—Tungsten Inert Gas.
Unlike other welding processes, TIG welding uses a non-consumable tungsten electrode to create the arc. The weld puddle is protected by an inert shielding gas, most commonly argon, to prevent contamination. A separate filler rod is added manually when needed, offering unmatched precision and control.
This welding method is widely used in Calgary for high-end fabrication, aerospace components, pressure piping, food-grade stainless equipment, and thin-gauge aluminum projects where appearance and structural integrity are critical.
Why TIG Welding Is Preferred in Calgary: Key Advantages
✔ 1. Superior Weld Quality and Appearance
TIG welding produces incredibly clean welds with no spatter, minimal smoke, and excellent bead appearance. This is ideal for visible structural elements such as railings, decorative metalwork, custom fabrication, and stainless steel assemblies.
✔ 2. Works on a Wide Range of Metals
TIG welding excels on:
Aluminum
Stainless steel
Mild steel
Titanium
Chromoly
Copper alloys
Nickel-based alloys
This versatility makes it valuable for industrial repair work across Calgary’s oil, gas, and energy sectors.
✔ 3. Ultimate Precision and Heat Control
Because the filler rod is added manually, the welder has full control of the:
Heat input
Weld puddle size
Bead shape
Penetration
This precision reduces distortion—especially important for thin materials, sheet metal, and aesthetic welds.
✔ 4. Strong, High-Integrity Welds
TIG welding creates a very strong, contamination-free weld, ideal for pressure-bearing or load-bearing structures.
How the GTAW (TIG) Welding Process Works
Below is a simplified but comprehensive breakdown of the TIG process used by professional welders in Calgary:
1. Material Preparation
TIG welding requires extremely clean surfaces. The welder prepares the metal by:
Removing oil, paint, rust, coatings
Cleaning with a stainless steel brush for aluminum
Wiping with acetone or alcohol
Ensuring tight, well-fitted joints
Proper preparation ensures stronger bonding and a cleaner weld bead.
2. Setting Up the Torch and Tungsten
The welder chooses the correct tungsten electrode type and diameter, such as:
2% Thoriated (Red) – common for DC mild steel and stainless
2% Lanthanated (Blue/Gold) – versatile for AC and DC
Pure Tungsten (Green) – older standard for AC aluminum
The electrode is sharpened to a precise point to control the arc shape.
3. Shielding Gas Flow (Usually Argon)
Pure argon (99.99%) is used in most Calgary fabrication applications because it:
Provides arc stability
Keeps the weld puddle clean
Prevents contamination
Flow rates generally range from 10–20 CFH, depending on cup size and welding conditions.
4. Establishing the Arc
The welder uses a foot pedal or fingertip control to ignite and regulate the arc. The tungsten does not touch the metal. This creates a focused heat zone for precision work.
5. Adding the Filler Material
When required, the welder dips a filler rod into the molten puddle, controlling:
Penetration
Strength
Weld bead shape
This allows for extremely clean, stacked-dime welds.
6. Final Pass and Shielding Coverage
Once the welder finishes the joint, the torch remains in place briefly to maintain gas shielding as the weld cools. This prevents:
Pitting
Oxidation
Color changes in stainless steel
Best Practices for High-Quality TIG Welding
Professional TIG welders follow several strict techniques to ensure top results:
🔧 Maintain Proper Tungsten Geometry
A sharp, uniform tungsten shape leads to:
Better arc stability
Cleaner puddle control
More consistent welds
🔧 Keep the Filler Rod Inside the Gas Shield
To avoid contamination, the filler metal must stay inside the gas coverage.
🔧 Control Heat Input
Too much heat causes distortion or burn-through, especially in thin aluminum or stainless.
🔧 Use the Correct Tungsten Type
Each metal requires a specific tungsten for optimal arc stability.
Tungsten type is marked by the colour band on the end of the electrode.
🔧 Maintain Cleanliness
Contaminants instantly ruin TIG weld quality — cleanliness is crucial.
Common TIG Welding Filler Rod Types (GTAW Wire Types)
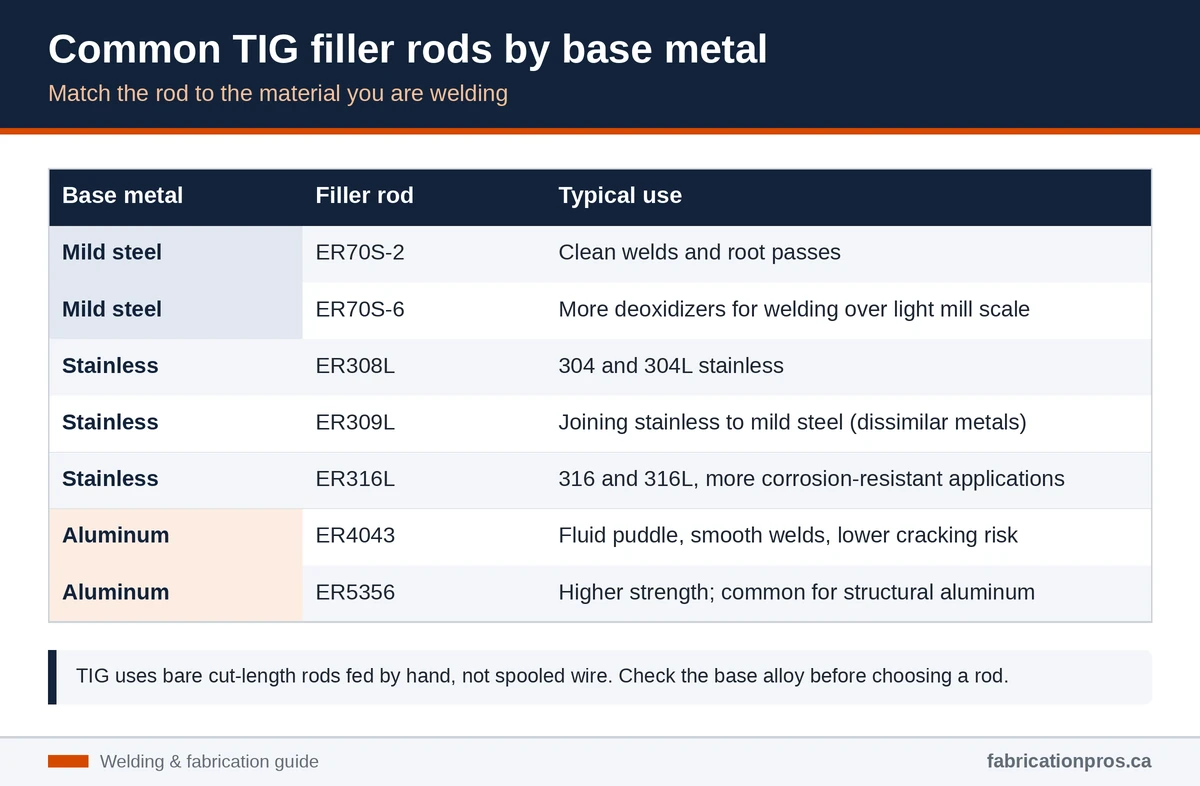
TIG welding uses bare filler rods, not spooled wire. Common types include:
For Mild Steel
ER70S-2 – Excellent for root passes and clean welds
ER70S-6 – Higher deoxidizers for welding over mill scale
For Stainless Steel
ER308L – For 304/304L stainless
ER309L – For dissimilar metals
ER316L – For 316/316L or corrosion-resistant applications
For Aluminum
ER4043 – Smooth, clean welds with lower cracking risk
ER5356 – Stronger, great for structural aluminum
For Exotic Metals
ER70S-2 Chromoly – For race car frames
CP Titanium Rods – Aerospace and corrosive environments
Nickel Alloy Rods (Inconel fillers) – High-heat, high-stress parts
Each filler metal is chosen based on strength, corrosion resistance, ductility, and compatibility with the base material.
Match the rod to the base metal before you strike an arc.
Common Applications of GTAW (TIG) Welding in Calgary
TIG welding is essential across multiple Calgary industries:
Looking for Professional TIG Welding Services in Calgary?
If your project requires:
High-precision welds
Stainless steel or aluminum fabrication
Clean, spatter-free welding
Industrial-grade repairs
Custom metal components
A professional TIG welder can deliver results that stand above other welding processes. TIG welding is the gold standard for durability, accuracy, and appearance—and the best choice for Calgary’s demanding industries.
MIG welding—also known as Gas Metal Arc Welding (GMAW)—is one of the most widely used welding processes in both industrial and commercial environments. Known for its speed, versatility, efficiency, and consistent weld quality, MIG welding is a go-to method for fabrication projects, automotive repair, construction, equipment repair, and general manufacturing.
In this in-depth guide, we break down how MIG welding works, the equipment involved, wire types, best practices, and the industries that rely on MIG welding every day. Whether you’re a beginner, a professional welder, or a business owner researching welding services, this article covers everything you need to know.
MIG (Metal Inert Gas) welding is a welding process where a spool-fed wire electrode is continuously fed through a welding gun, where it melts and fuses the metal surfaces together. Unlike stick welding, which uses a consumable electrode rod, MIG welding uses a wire and shielding gas to protect the weld from contamination.
This results in:
Clean, smooth welds
Faster travel speeds
Less spatter
Minimal welding fumes
Easier learning curve for beginners
Because of its efficiency and adaptability, MIG welding is one of the most commonly used welding methods worldwide.
How MIG Welding Works
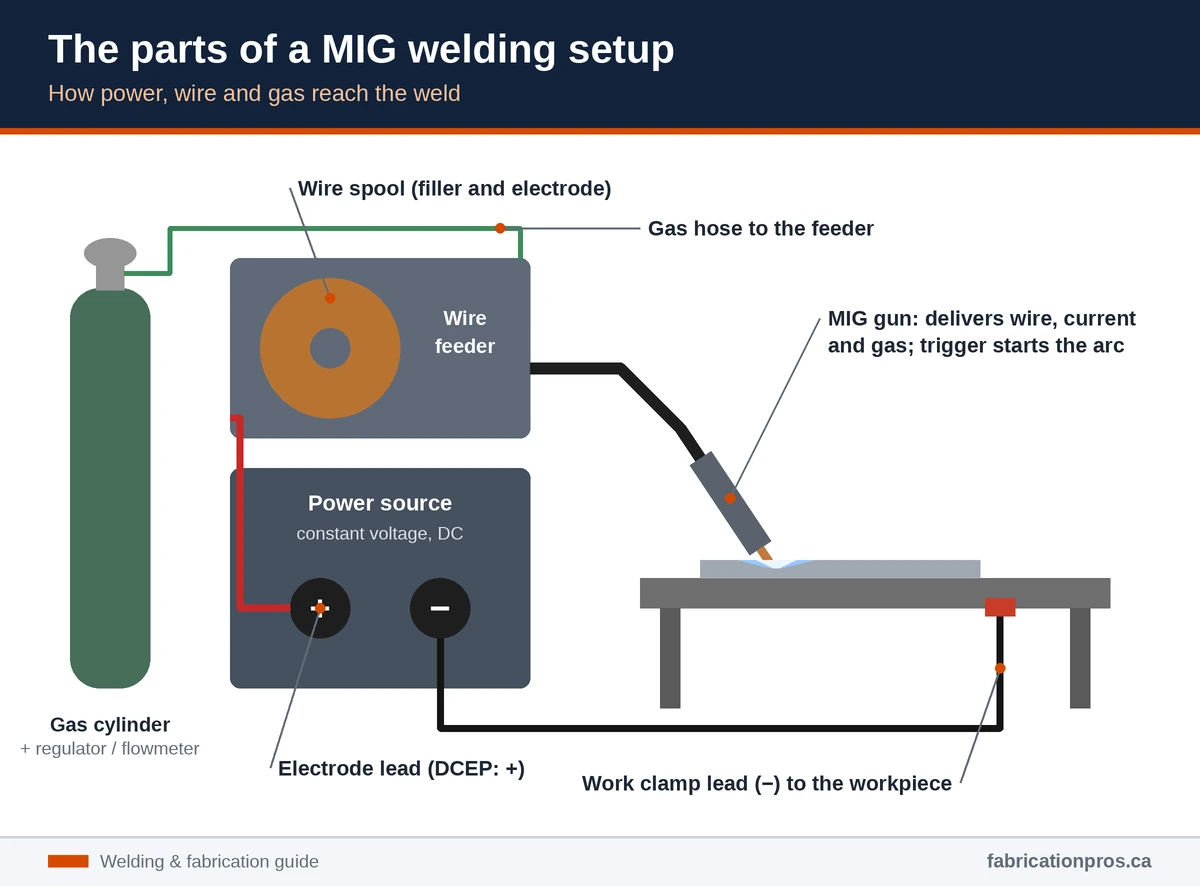
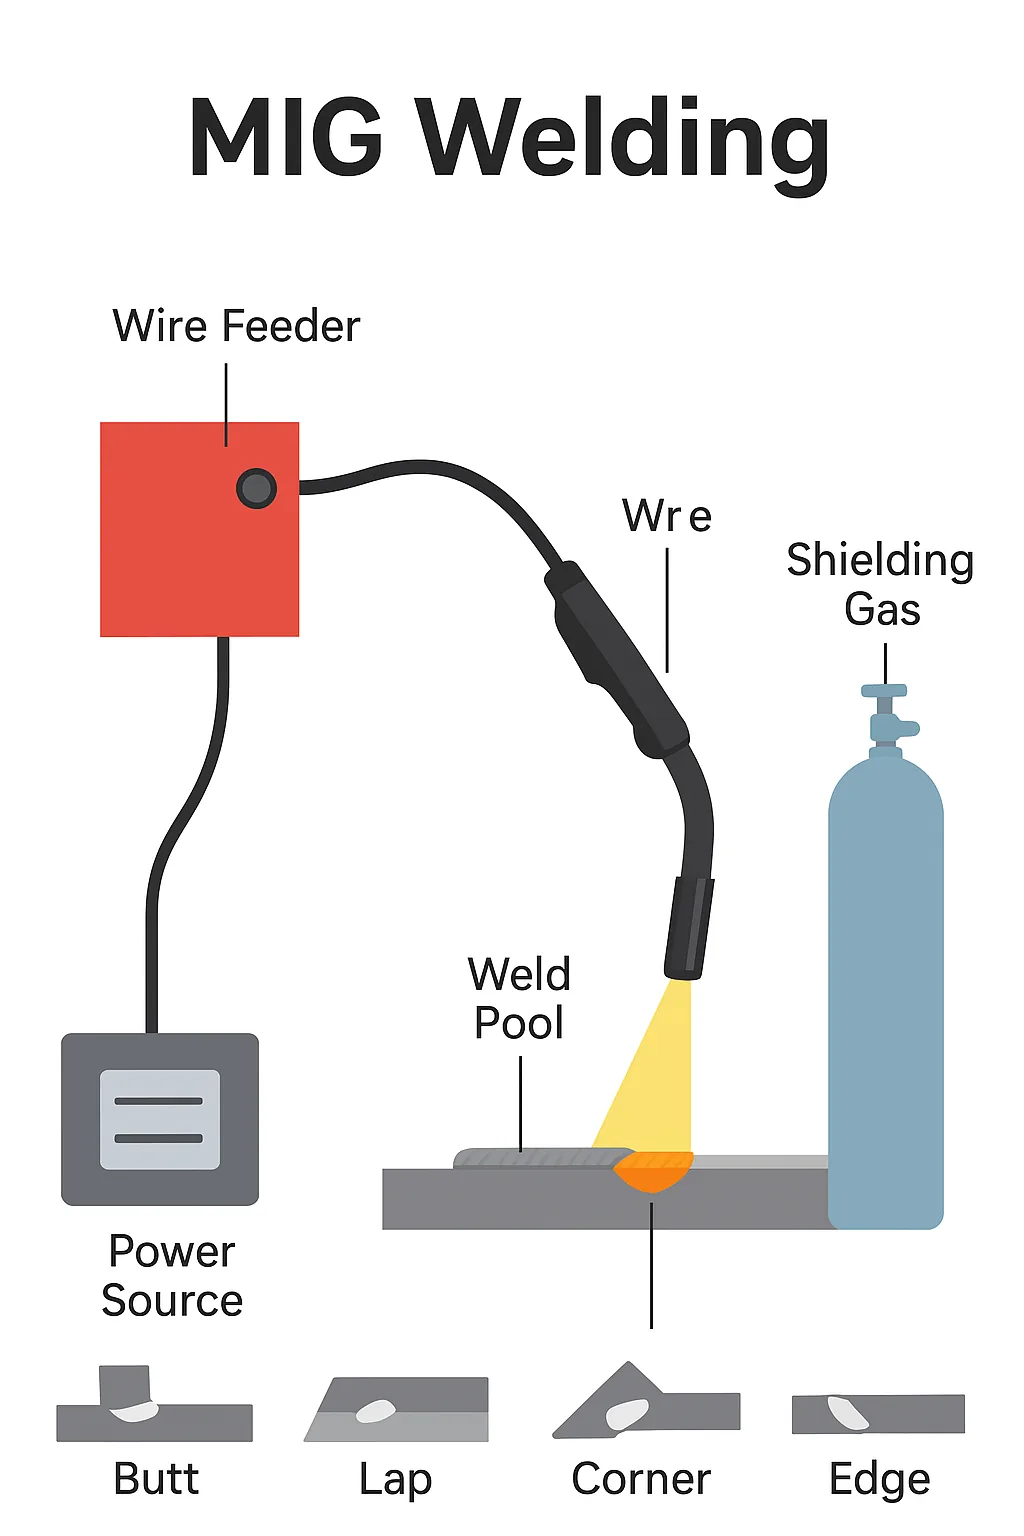
The MIG process relies on four main components working together:
1. Power Source
The machine provides a constant voltage, usually DC+, which stabilizes the arc and ensures consistent deposition.
2. Wire Feeder
A motorized wire feeder pushes welding wire through the MIG gun at a controlled, adjustable speed. The wire acts as:
Filler material
Electrode
3. MIG Gun
The MIG gun delivers:
The wire electrode
Electrical current
Shielding gas
A trigger controls the wire feed and arc initiation.
4. Shielding Gas
A blend of gases protects the weld pool from atmospheric contamination. Common gases include:
C25 (75% Argon, 25% CO₂) – Most common for mild steel
100% CO₂ – Deep penetration, more spatter
100% Argon – Aluminum and non-ferrous metals
Argon/Helium Mixes – Stainless steel and specialty metals
The shielding gas is crucial—without it, the weld suffers from porosity, poor fusion, and contamination.
How power, wire and shielding gas reach the weld.
Advantages: MIG Welding
MIG welding offers several benefits, making it popular across industries:
✔ Fast welding speeds
Perfect for production and fabrication shops.
✔ Easy for beginners to learn
MIG is more forgiving and easier to control than TIG or stick welding.
Whether you’re repairing heavy equipment, fabricating new steel structures, or working with aluminum, MIG welding offers unmatched speed, versatility, and performance. With the right wire, gas, settings, and technique, MIG welding produces durable welds suitable for nearly every industry.
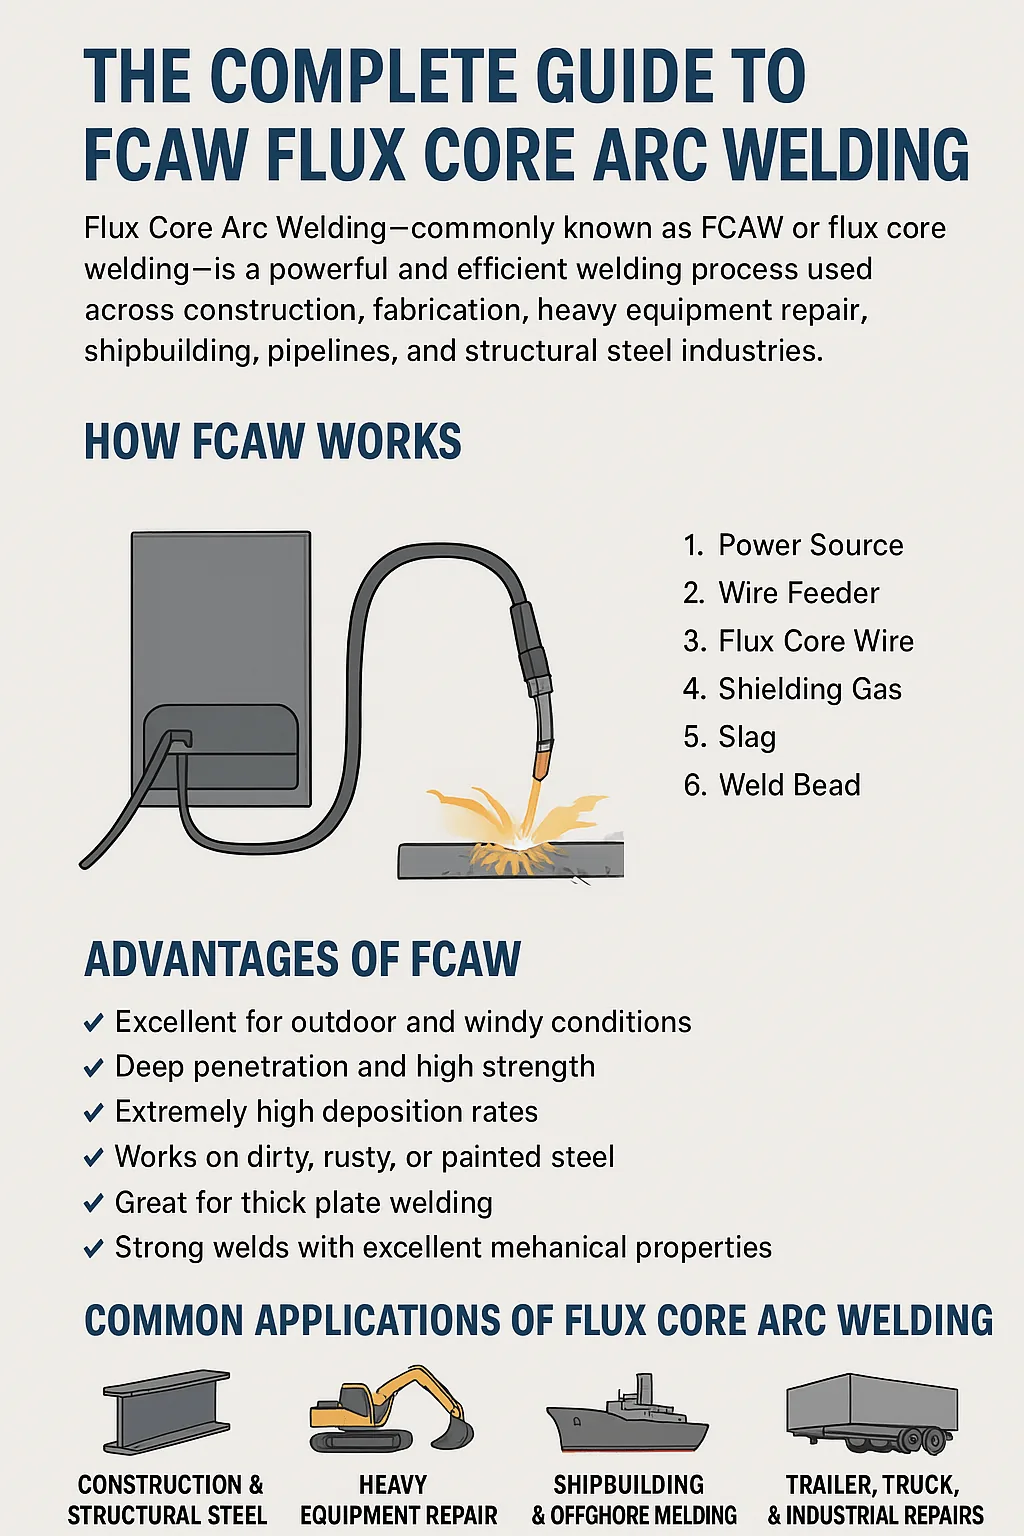
Flux Core Arc Welding—commonly known as FCAW or flux core welding—is one of the most powerful and efficient welding processes used across construction, fabrication, heavy equipment repair, shipbuilding, pipelines, and structural steel industries. Known for its high penetration, deep fusion, and ability to weld outdoors in windy conditions, FCAW is a top choice for welders who demand strong, durable welds even in challenging environments.
In this comprehensive guide, we break down everything you need to know about FCAW, including how the process works, the different types of flux-core wire, ideal applications, machine setup, and best practices used by certified red seal welding professionals.
Flux Core Arc Welding (FCAW) is a semi-automatic welding process that uses a continuously fed consumable wire containing a flux compound in its core. The flux reacts under heat to create shielding gases and slag, protecting the weld from contamination.
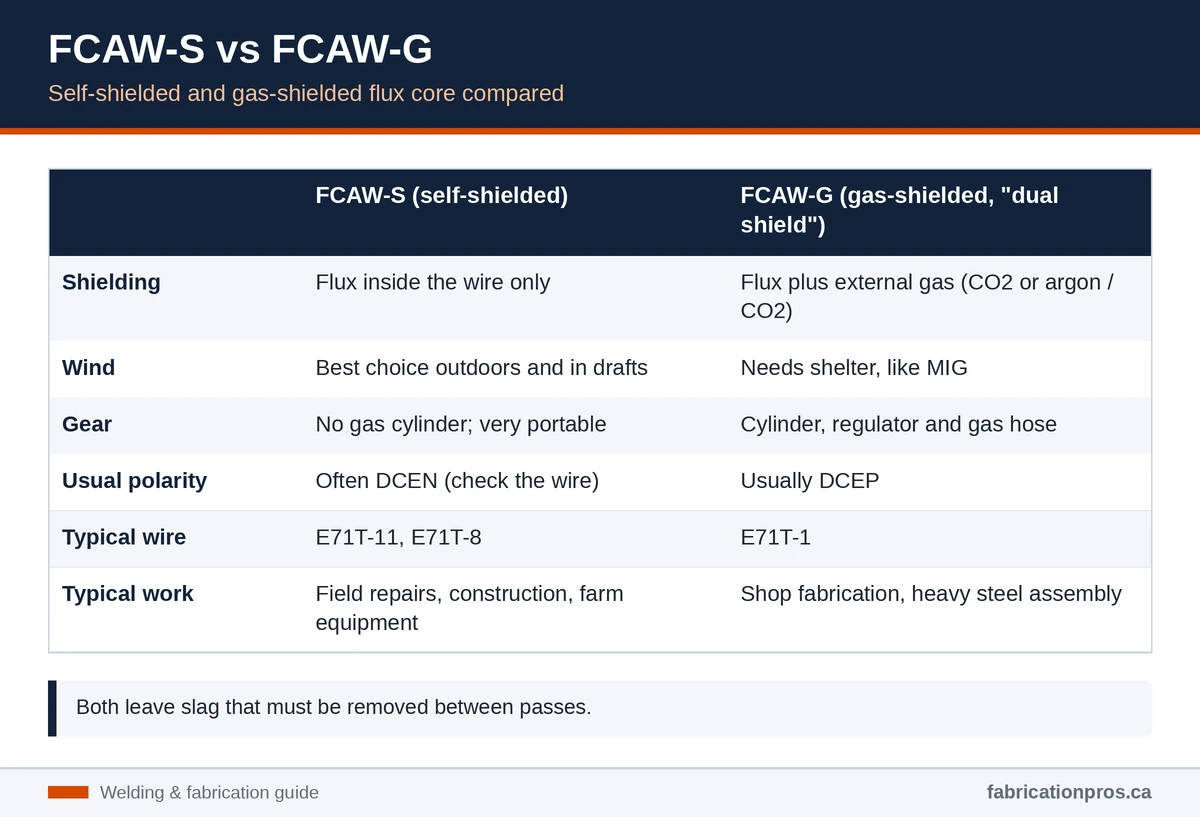
FCAW is similar to MIG welding, except FCAW uses flux-filled wire instead of solid wire and can be used with or without external shielding gas:
It’s the ideal combination of power, durability, productivity, and versatility—making FCAW one of the most relied-on welding processes in industrial environments.
Final Thoughts: FCAW Remains One of the Strongest and Most Reliable Welding Methods
Whether used on construction sites, in manufacturing facilities, or in heavy equipment repair, Flux Core Arc Welding delivers unmatched performance and strength. Its ability to handle dirty metal, weld outdoors, and penetrate thick steel makes it indispensable to welders who need results that last.
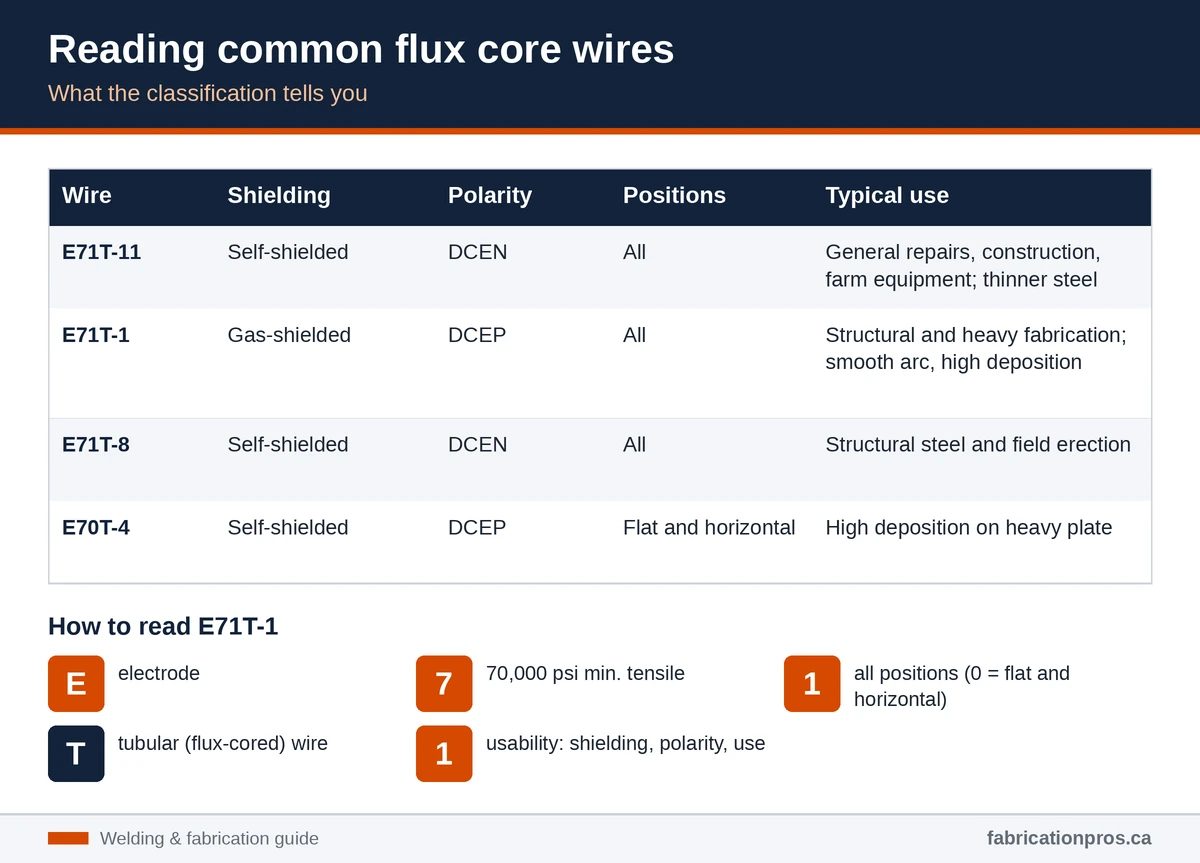
Polarity matters with flux-cored wire too: most gas-shielded wires run on DCEP, while many self-shielded wires run on DCEN, so check the wire manufacturer’s data sheet before you start. Our article on straight vs reverse polarity in welding explains how each setting changes heat and penetration.
When it comes to welding, whether you’re working on aluminum fuel tanks, structural steel, or heavy equipment — understanding welding polarity is essential for strong, clean, and efficient welds. At Fabrication Pros we get asked: What’s the difference between straight and reverse polarity — and which one should I use?
In this post, we’ll break down the science behind welding polarity and explain how it affects penetration, bead profile, and weld quality.
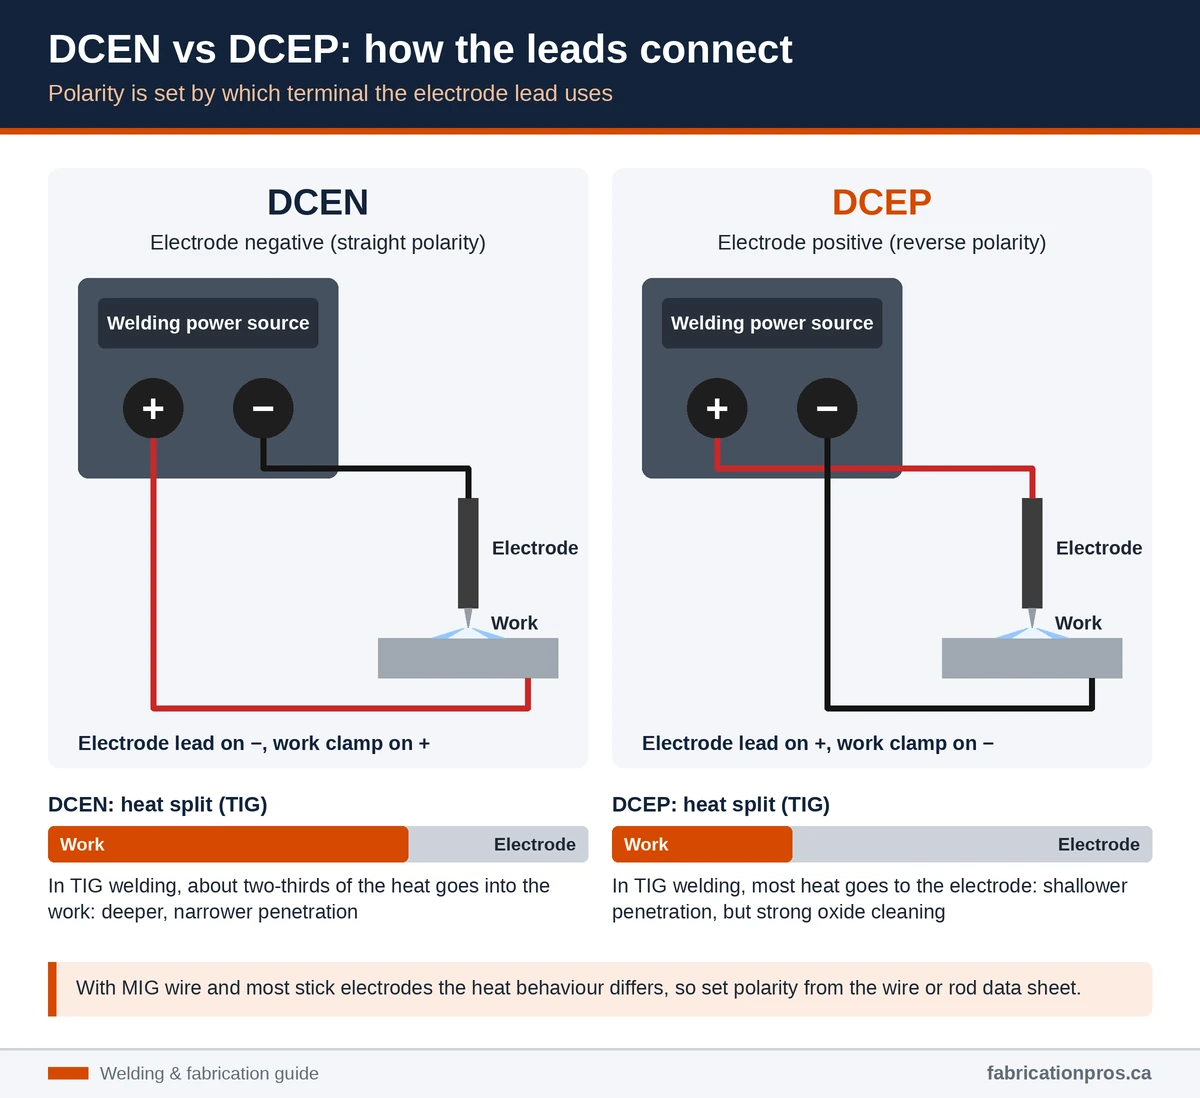
Welding polarity refers to the direction of current flow in a welding circuit. In any DC (direct current) welding setup, electricity flows from the negative terminal to the positive terminal. By switching which side the electrode connects to, welders can change how heat is distributed between the electrode and the workpiece.
There are two main types of polarity used in DC welding:
Straight Polarity (DCEN) – Direct Current Electrode Negative
Reverse Polarity (DCEP) – Direct Current Electrode Positive
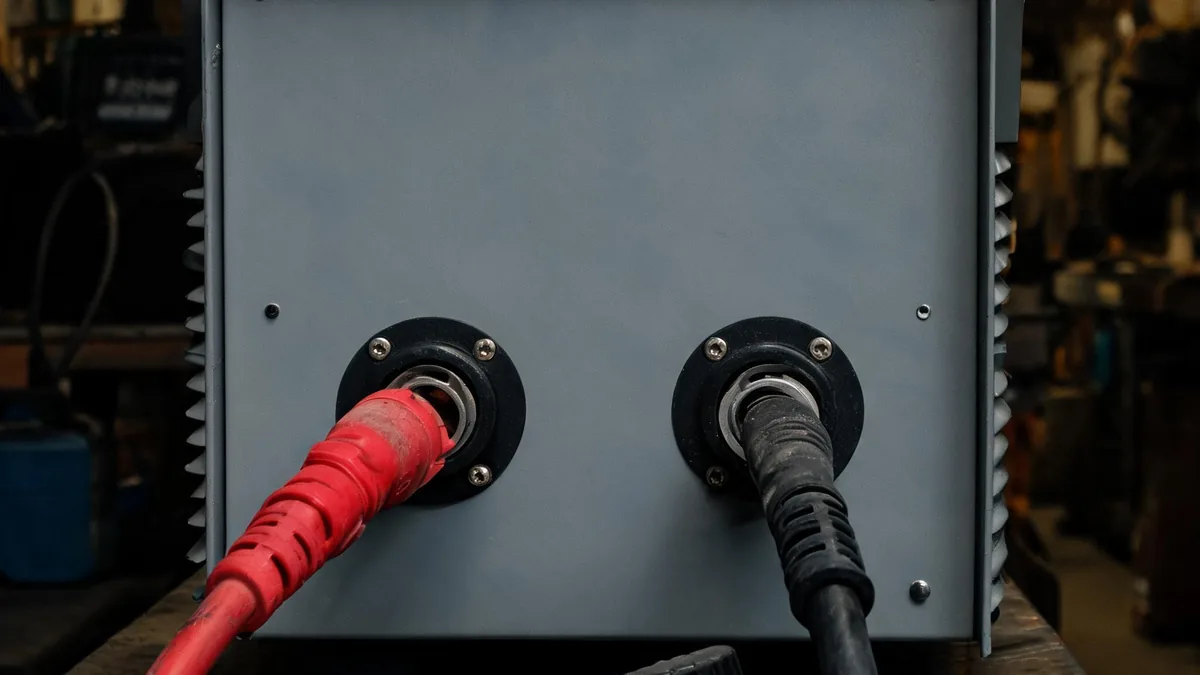
Polarity is simply which terminal the electrode lead is connected to.
Straight Polarity (DCEN) – Deep Penetration for Heavy Welding
In straight polarity, the electrode is negative and the workpiece is positive. About two-thirds of the heat is concentrated on the workpiece, providing deeper penetration and faster material fusion.
✅ Best For:
TIG (GTAW) welding stainless steel and carbon steel (aluminum is TIG welded on AC; see the note below)
Thicker materials
Pipe welding and structural applications
⚡ Key Benefits:
Deep weld penetration
Faster travel speeds
Less electrode consumption
⚠️ Things to Watch:
Can produce a narrower bead
Not ideal for thin materials (risk of burn-through)
🔄 Reverse Polarity (DCEP) – Cleaner Welds and Better Fusion
In reverse polarity, the electrode is positive, and the workpiece is negative. This reverses the heat distribution — now, most of the heat is concentrated on the electrode tip. The result is shallower penetration but better surface cleaning due to the electron flow that removes surface oxides.
The right polarity depends on the material type, thickness, and welding process:
Welding Process
Recommended Polarity
Typical Use
TIG (GTAW)
Straight Polarity (DCEN)
Stainless, carbon steel, precision work (aluminum uses AC)
MIG (GMAW)
Reverse Polarity (DCEP)
General fabrication, automotive, sheet metal
Stick (SMAW)
Depends on Electrode Type
Varies by rod type (E6010 uses DCEP, E6013 can use both)
A note on aluminum: TIG welding aluminum is normally done on alternating current (AC), not DCEN. AC switches between the two polarities many times per second: the electrode-positive half breaks up aluminum’s oxide layer and the electrode-negative half provides penetration. Our guide on why aluminum welding is different from steel explains more.
If you’re unsure which polarity to use, consult your electrode manufacturer’s datasheet or reach out to an experienced welding technician — using the wrong polarity can cause weak welds, excess spatter, or porosity.
Start with the process, then confirm on the wire or electrode data sheet.
Calgary’s Trusted Welding Experts Explain How to Choose the Right Filler Metal
Overview
When welding aluminum, choosing the right electrode or filler rod can make all the difference in the strength, appearance, and performance of your weld. For welders and fabricators in Calgary, Alberta, two of the most common choices are 5356 aluminum electrodes and 4043 aluminum electrodes.
While they may look similar, these two filler metals behave very differently — and choosing the wrong one for your application can lead to cracking, corrosion, or weak joints. At Fabrication Pros, Calgary’s local mobile and rig welding specialists, we’re breaking down the key differences between 5356 and 4043 aluminum to help you make the right choice for your project.
Aluminum is lightweight, strong, and corrosion-resistant — but it’s also one of the more challenging metals to weld. Different aluminum alloys require specific filler materials that match or complement their composition.
That’s why choosing between 5356 and 4043 aluminum filler metals isn’t just about preference — it’s about ensuring weld integrity and long-term performance.
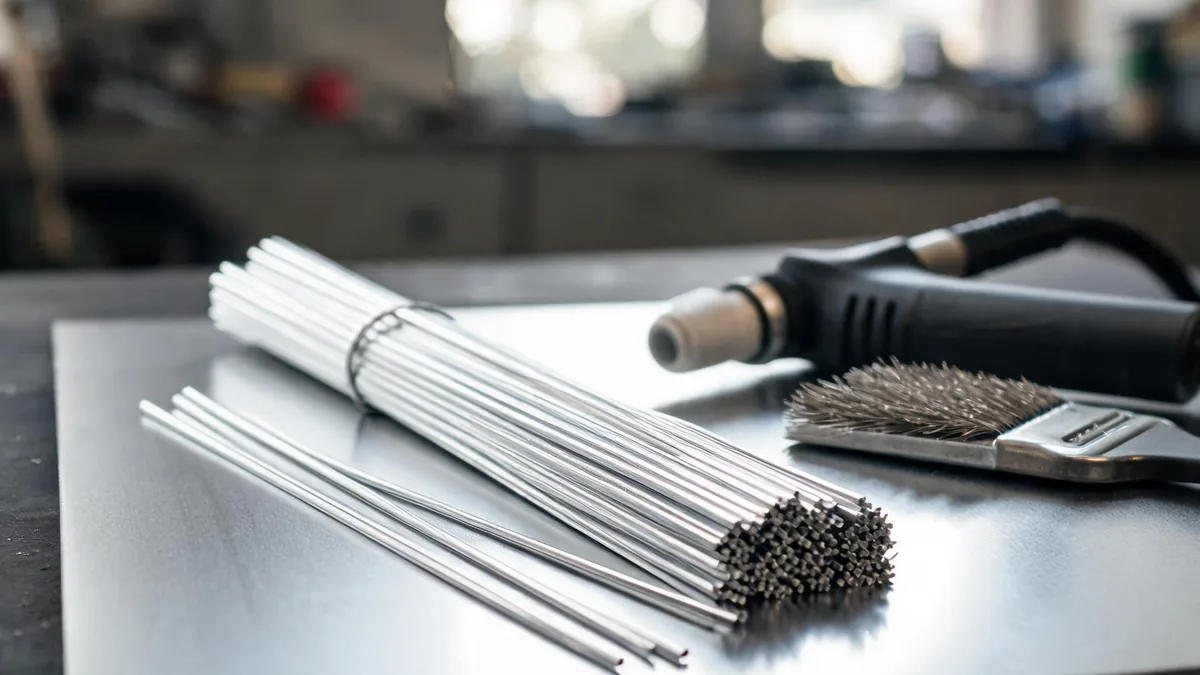
Aluminum filler rods look alike, so keep them labelled: 4043 and 5356 behave very differently.
4043 Aluminum Electrodes: The Go-To for General Aluminum Welding
4043 is one of the most widely used aluminum filler materials in welding. It’s an aluminum-silicon alloy, containing around 5% silicon, which gives it excellent flow characteristics and crack resistance.
Key Benefits of 4043 Aluminum:
Excellent fluidity — easier to work with for smooth, clean weld beads
Reduced cracking risk due to added silicon
After anodizing, a darker gray/charcoal finish than the surrounding aluminum; 5356 usually gives a closer color match
Compatible with 3000, 4000, 6000 series aluminum alloys
Ideal for welding 6061 aluminum and other 6xxx alloys
4043 is often useful for general aluminum welding on compatible alloys because of its fluid weld pool and relatively low hot-cracking tendency on many 6xxx alloys — a major advantage for custom fabrication and repair work.
5356 Aluminum Electrodes: Designed for Strength and Corrosion Resistance
5356 aluminum filler metal is an aluminum-magnesium alloy, containing about 5% magnesium. It’s specifically engineered for high-strength, corrosion-resistant welds, especially in marine or outdoor applications.
Key Benefits of 5356 Aluminum:
Superior strength compared to 4043
Outstanding corrosion resistance, especially in saltwater or harsh environments
Higher strength and typically higher ductility than 4043 weld metal, where compatible with the base alloy and service conditions
Compatible with 5052, 5083, 5652, and other magnesium-bearing alloys
However, it’s important to note that 4043 often has a lower hot-cracking tendency on 6xxx alloys such as 6061, while 5356 is commonly selected where higher weld strength or a closer anodized color match is needed. Check the base alloy and application before choosing.
The Key Difference Between 4043 and 5356
Feature
4043 Aluminum
5356 Aluminum
Alloy Type
Aluminum-Silicon
Aluminum-Magnesium
Strength
Moderate
High
Corrosion Resistance
Good
Excellent
Crack Resistance
Excellent
Moderate
Ductility
Generally lower
Typically higher
After anodizing
Often dark gray/charcoal; poor color match
Generally closer color match to the base metal
Typical Applications
General fabrication, automotive
Marine, transport, structural
As-welded appearance
Smooth, bright
Slightly duller, stronger bead
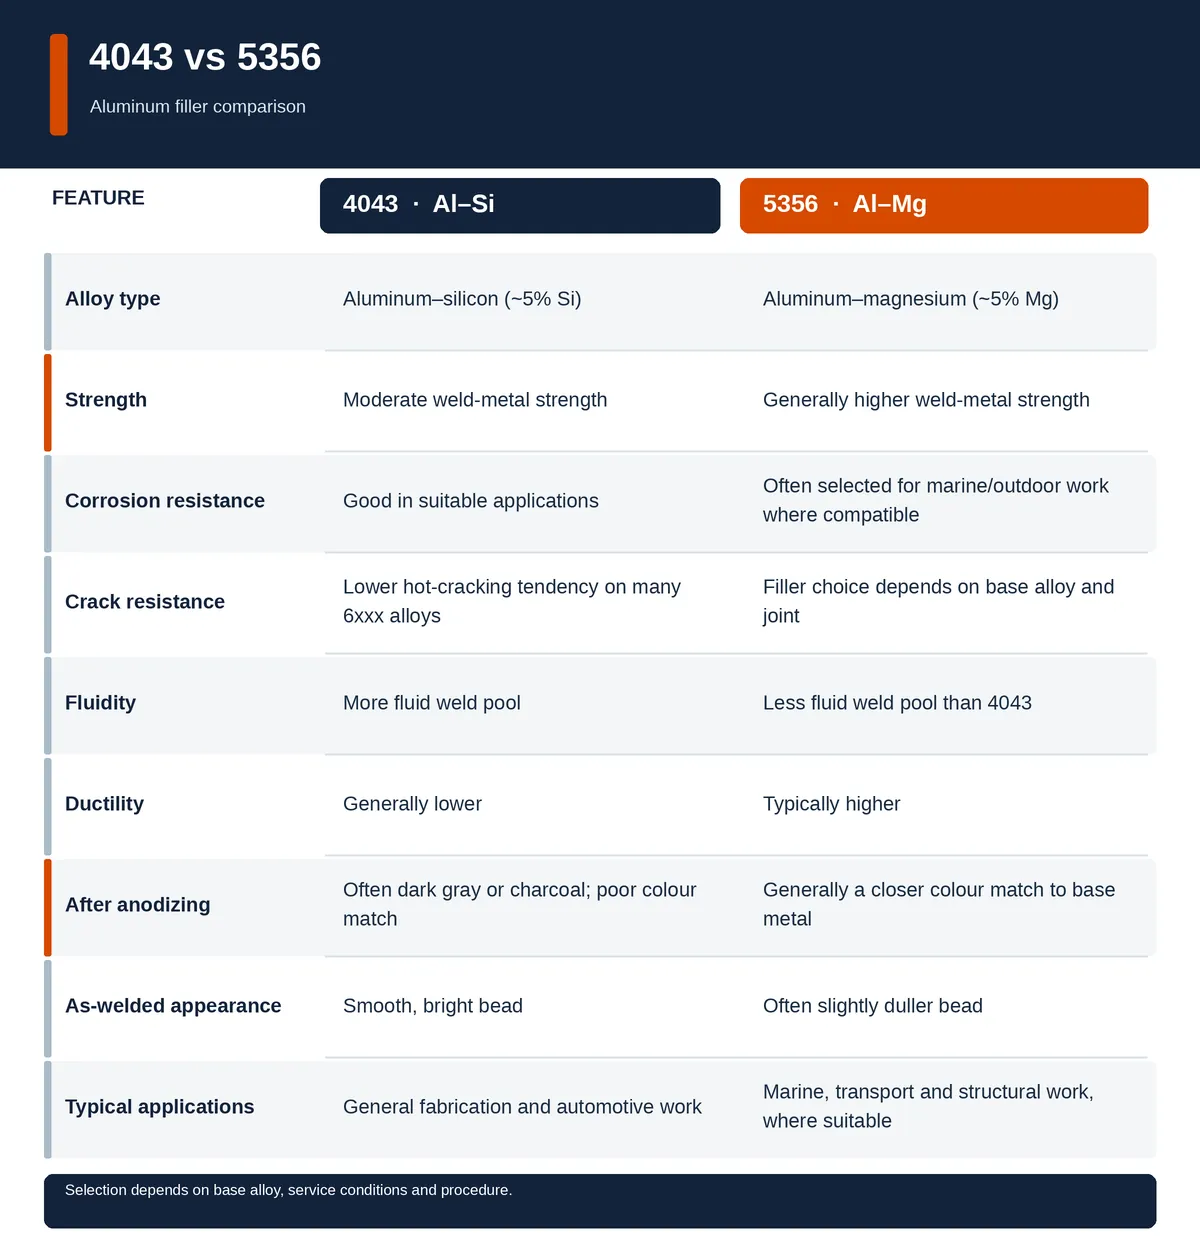
4043 and 5356 filler comparison, including strength, fluidity, ductility and anodized colour. Match filler to the base alloy and service conditions.
Choosing the Right Electrode for Your Job
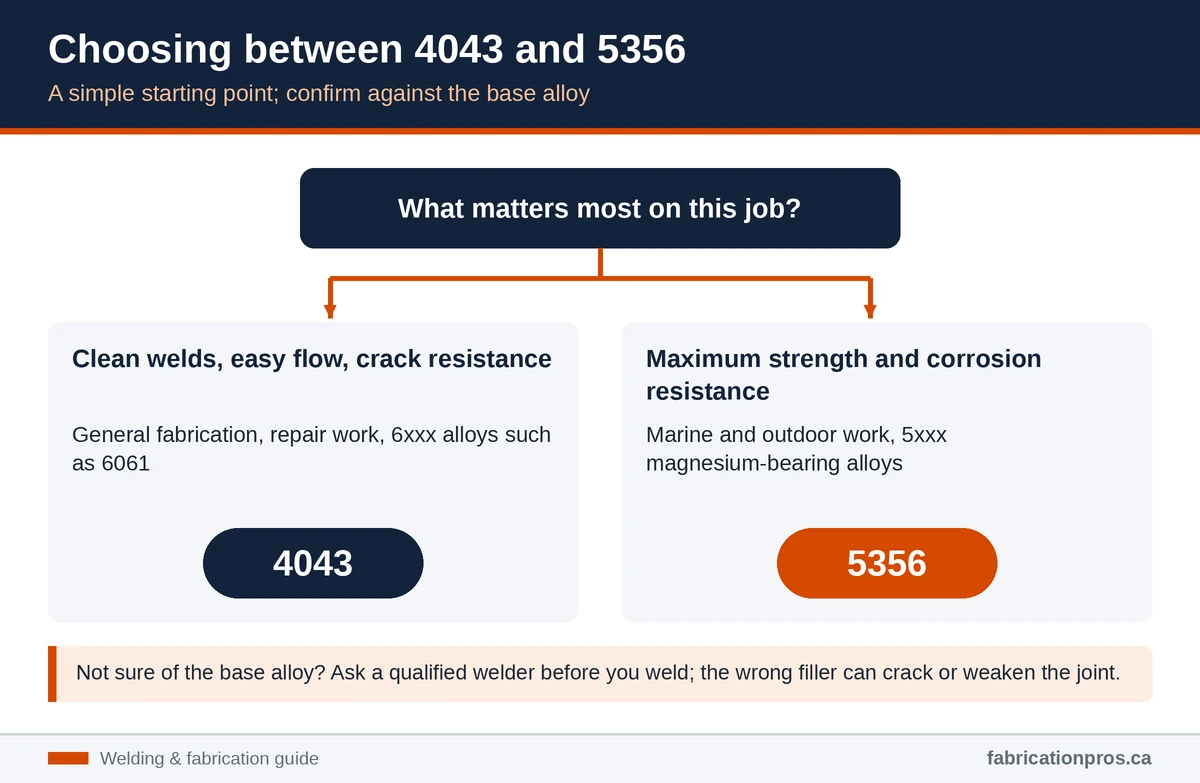
If your project requires maximum strength and corrosion resistance, especially in marine or outdoor environments, 5356 aluminum electrodes are your best choice.
If you’re working on general fabrication, repair work, or welding 6xxx series aluminum, 4043 electrodes will give you cleaner welds, easier workability, and better crack resistance.
When in doubt, consult a qualified welder or welding engineer who understands how filler metal selection affects performance, especially under Alberta’s tough working conditions.
A starting point; always confirm against the base alloy.
Our certified rig welders use the right electrodes, processes, and techniques for your specific alloy and application — ensuring strong, clean, and long-lasting welds every time.
What Is SMAW Welding? A Complete Guide to Stick Welding
Short answer
SMAW welding, short for Shielded Metal Arc Welding, is one of the most common and dependable welding processes used in the industry today. Often referred to as stick welding, SMAW is known for its versatility, strength, and reliability — making it ideal for structural steel, repair work, and outdoor projects.
In SMAW welding, an electrode coated in flux is used to carry the electric current that creates an arc between the electrode and the base metal. This arc generates intense heat, which melts both the electrode and the workpiece to form a solid weld joint.
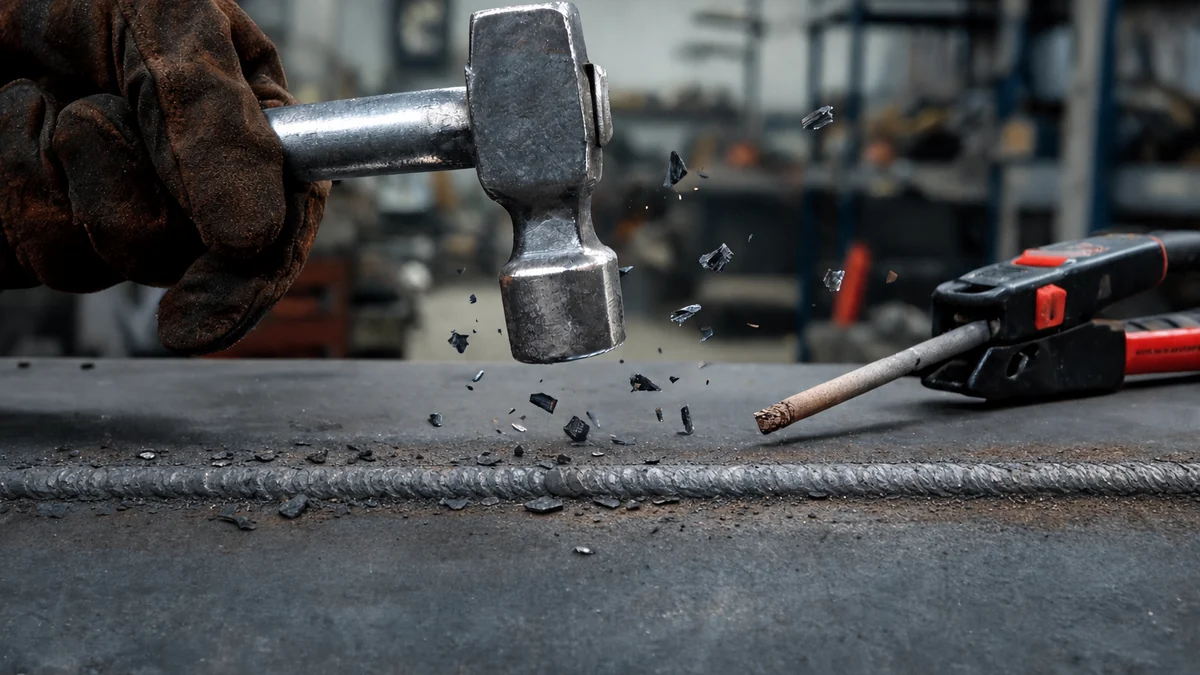
As the electrode melts, the flux coating releases shielding gases and forms a layer of slag over the weld. This protective layer prevents contamination from oxygen and moisture, ensuring a strong, clean weld once the slag is removed.
Because SMAW does not rely on external shielding gas, it performs exceptionally well in outdoor or windy conditions where other welding methods might struggle.
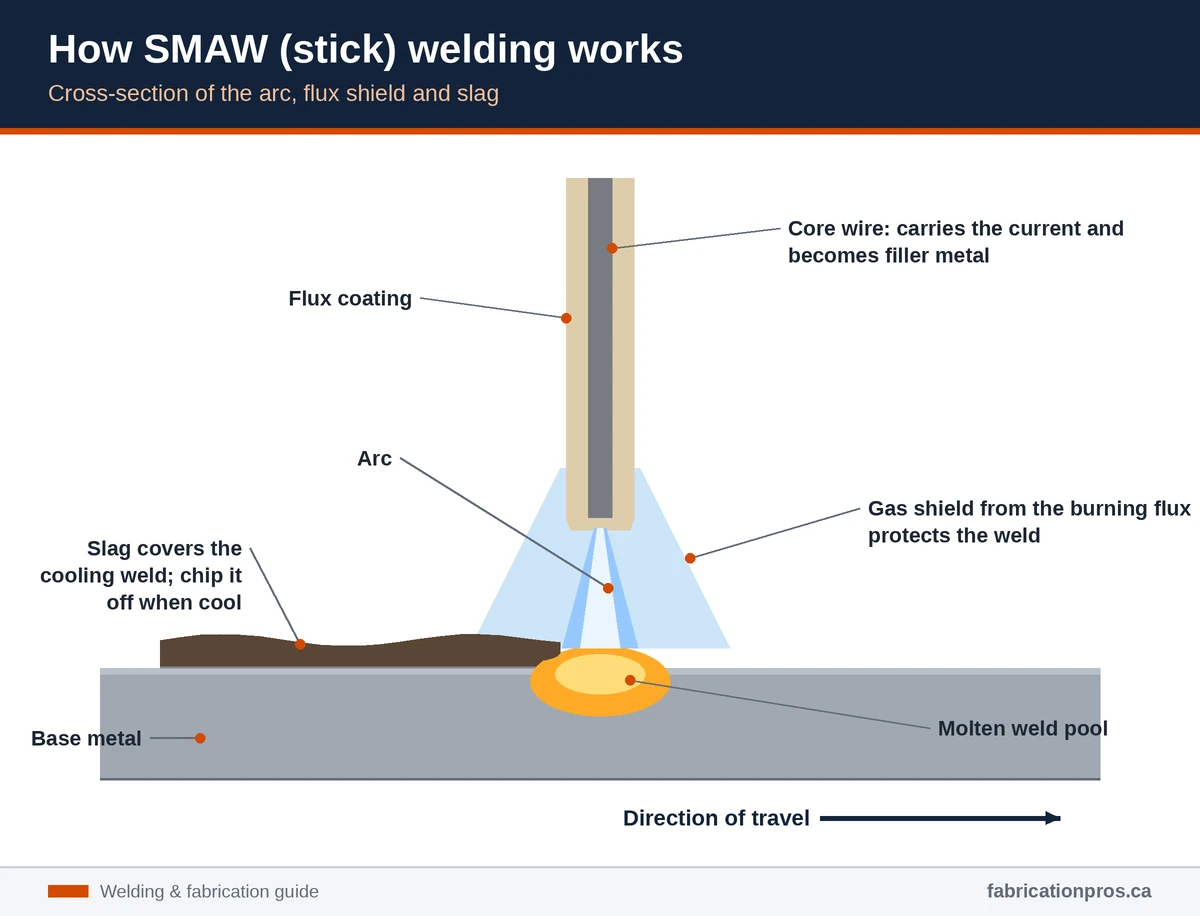
The burning flux makes the gas shield and the slag that protect the weld.
Advantages of SMAW Welding
SMAW remains one of the most popular welding techniques worldwide due to its durability and flexibility. Some of its top advantages include:
✅ Versatile Applications: Works on a wide range of metals, including steel, stainless steel, cast iron, and alloy steel.
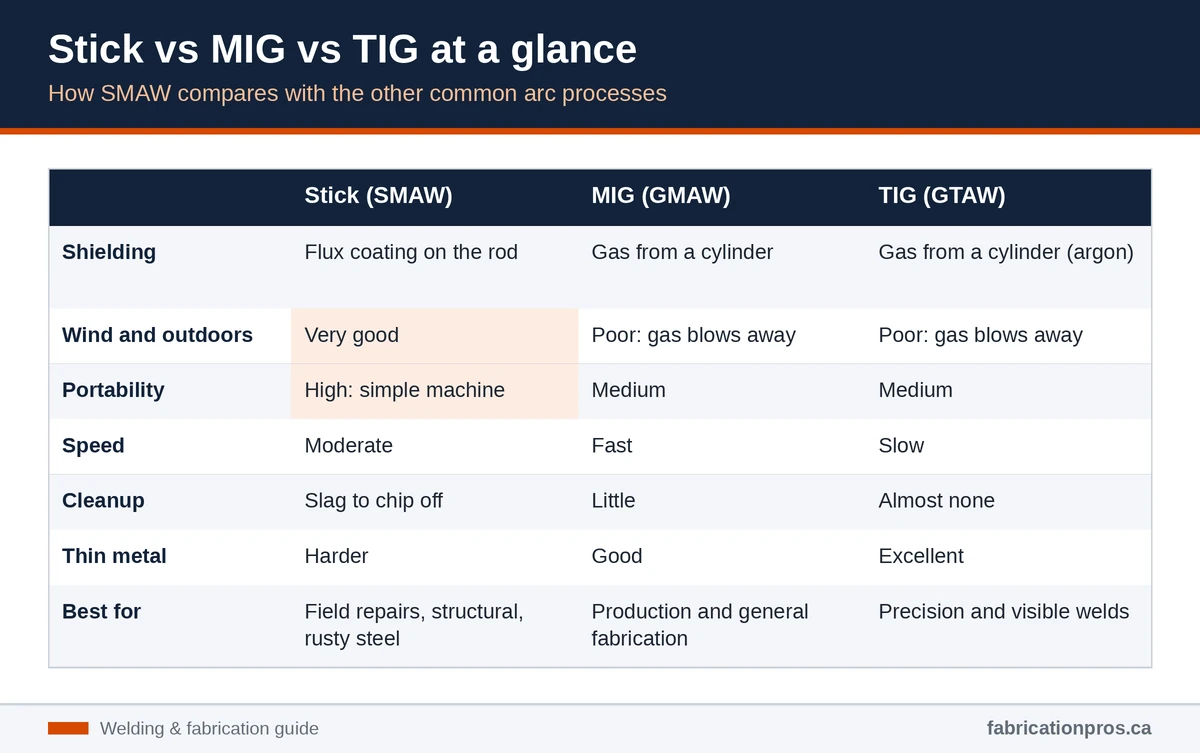
Compared to GMAW (MIG welding) and GTAW (TIG welding), SMAW is more portable and better suited for heavy-duty work in challenging environments. While MIG and TIG produce cleaner and more precise welds, SMAW excels in strength, simplicity, and versatility — especially for repairs, construction, and outdoor applications.
At Fabrication Pros, we provide professional SMAW welding servicesin Calgary for industrial, commercial, and structural projects. Our experienced welders deliver durable, high-quality welds that meet exact safety and performance standards — whether you need on-site repairs or new fabrication work.